ULVAC, Inc.
Similar suppliers you may like
Volkmann, Inc.
🇺🇸 United States
200811-50 peopleManufacturer/Service CompanyOEM manufacturer
Product customization
Patented technology
Industry association member
Shipments
276
Key customer
SAFTEK
Key market
🇹🇷 Turkey
Description
Volkmann, Inc. is a US-based manufacturer and service company specializing in high-quality, high-performance pneumatic vacuum conveyors and powder process equipment. Established in 2008 as a subsidiary of the global Volkmann GmbH, the company operates with 11-50 employees from its Bristol, PA facility, which includes a 750 square foot dedicated test laboratory for material testing and custom solution design. Volkmann, Inc. offers OEM and contract manufacturing services, providing fully contained powder and bulk material handling systems designed for safe, dust-tight, damage-free, gentle, and dense phase conveying of powders and dry solids under vacuum. Their product range includes pneumatic vacuum conveyors (VS Series, PPC Series for pharmaceuticals, INEX Series), bulk bag unloaders, rip and tip stations, weighing and dosing systems, and specialized additive manufacturing systems like the PowTReX for metal powder recovery. A key innovation is their patented Multijector® vacuum pump technology, which generates suction without heat or rotating parts. All systems are ATEX and UL certified, ensuring explosion-proof operation. Volkmann, Inc. serves diverse industries including food, pharmaceuticals, chemicals, and additive manufacturing, providing both standard equipment and customized solutions for complex applications.
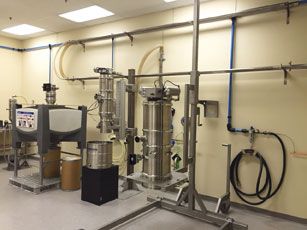
Volkmann's testing laboratory in Bristol, PA, features full-size, fully operational bulk material handling equipment.
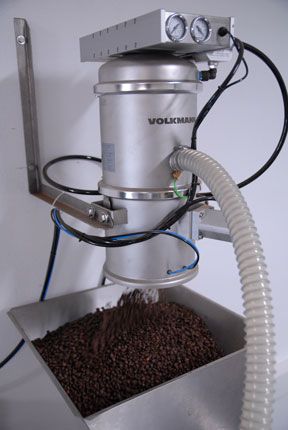
Volkmann pneumatic vacuum conveyor that discharges coffee
UL Certified red logo for Volkmann controllers

ATEX logo documents explosion-proof Volkmann conveyors
Volkmann's testing laboratory in Bristol, PA, features full-size, fully operational bulk material handling equipment.
Volkmann pneumatic vacuum conveyor that discharges coffee
Volkmann brochure list of Conveyable Materials experience
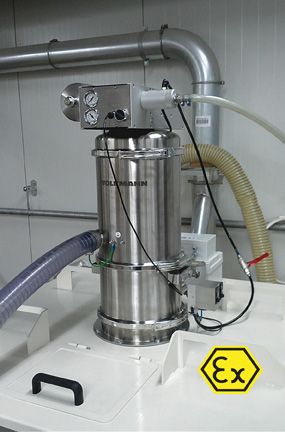
Volkmann pneumatic vacuum conveyors are ATEX certified and explosion-proof by design.
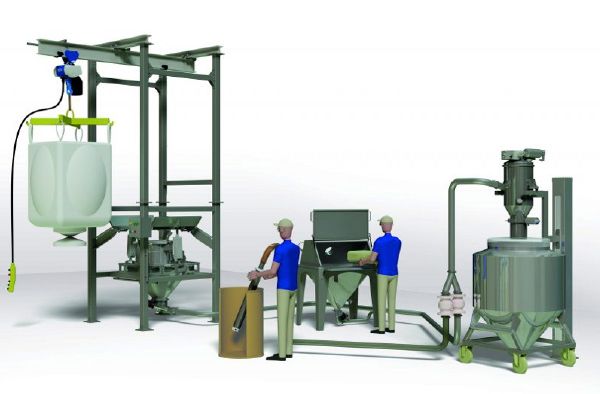
Illustration of the Volkmann pneumatic vacuum conveyor system with bulk bag discharger and suction lance
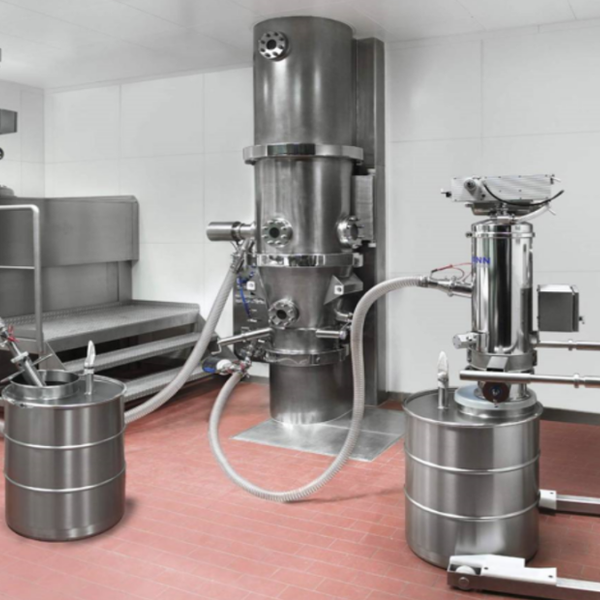
Volkmann pneumatic vacuum conveyor system
Pneumatic Vacuum Conveyors
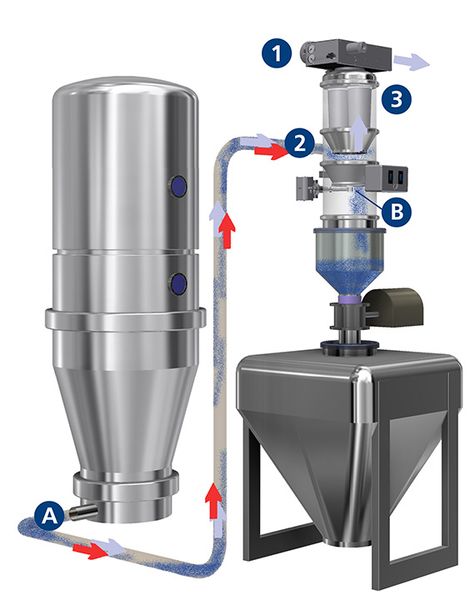
Diagram of how Volkmann pneumatic vacuum conveyors work

COVAL Vacuum Technology, Inc.
🇺🇸 United States
198611-50 peopleManufacturer/Service CompanyEstablished brand
Product customization
OEM manufacturer
Shipments
68
Key customer
EMI
Key market
🇲🇽 Mexico
Description
COVAL Vacuum Technology, Inc. is a specialized manufacturer and service provider of vacuum handling solutions and automation components. Headquartered in Raleigh, North Carolina, the company serves as the US entity of the global COVAL Group, bringing over 35 years of expertise to the industrial automation sector. As an ISO 9001:2015 certified organization, COVAL positions itself as a "Vacuum Manager," offering a comprehensive portfolio that includes vacuum grippers, suction cups, vacuum pumps, and sophisticated End of Arm Tooling (EOAT). Their product range features advanced technologies such as the CVGL and MVG series grippers, carbon vacuum grippers, and the MPXS series of communicating micro vacuum pumps equipped with IO-Link and Air Saving Control (ASC) technology, which can reduce energy consumption by up to 90%. COVAL provides both standard components and custom-engineered solutions for diverse industries, including packaging, food processing, plastics, electronics, and pharmaceuticals. Their systems are designed to handle a wide variety of materials, from airtight parts to porous packaging like bags and pouches, with weight capacities ranging from under 15 kg to over 225 kg. By integrating intelligent vacuum generators and modular peripheral devices, the company helps global clients optimize production efficiency, enhance workplace safety, and reduce noise levels in automated environments.
Special Purpose Suction Cups