RICHTER Chemie-Technik GmbH
Similar suppliers you may like
CHT Germany GmbH
🇩🇪 Germany
19532001-5000 peopleManufacturer/Service CompanyHigh capacity factory
Established brand
Large enterprise group
Eco-friendly supplier
Shipments
16888
Key customer
CHT
Key market
🇵🇰 Pakistan
Description
CHT Germany GmbH, headquartered in Tübingen, is a globally active manufacturer and service provider specializing in innovative specialty chemicals. Founded in 1953, the company has grown into a medium-sized global player with approximately 2,500 employees across 27 companies, serving customers in over 120 countries. As a foundation-owned organization, CHT focuses on sustainable chemical solutions and long-term corporate responsibility, maintaining manufacturing plants and technical laboratories in Germany, Austria, the UK, Italy, China, and North America.
The company's extensive portfolio is divided into two primary segments: Textile Solutions and Industry Solutions. The Textile division provides a comprehensive range of auxiliaries for pretreatment, dyeing, printing, and finishing, alongside specialized textile care detergents for industrial laundries. Their Industry Solutions segment, branded under Silicone Experts, offers high-performance materials including silicone elastomers, adhesives, encapsulants, and moulding rubbers. These products serve diverse sectors such as automotive, aerospace, electronics, personal care, agriculture, and construction.
CHT is recognized for its technical capabilities in developing 1-part and 2-part silicone compounds and advanced enzyme technology for the paper industry. The company holds several sustainability certifications and commitments, including EcoVadis, the UN Global Compact, and SBTi. Notable innovations like the PIGMENTURA dyeing concept demonstrate their focus on resource-saving technologies that reduce CO2 emissions and water consumption. With over 70 years of experience, CHT Germany GmbH operates as a preferred partner for OEM and processed material requirements worldwide.
Ricite (Zhejiang) Science and Technology Co., Ltd.
🇨🇳 China
2018201-300 peopleManufacturerOwn brand
High-tech enterprise
Low MOQ
Key market
North America
Description
Ricite (Zhejiang) Science and Technology Co., Ltd. is a high-tech manufacturer of pump systems and valve products, established in 2018 in Huzhou, China, with 200 to 300 employees. The company specializes in the R&D, design, and manufacturing of high-quality, leak-free pumps, particularly magnetic pumps and diaphragm pumps. Their extensive product portfolio includes stainless steel magnetic pumps, fluorine-lined magnetic pumps, canned motor pumps, pneumatic diaphragm pumps, and electrical diaphragm pumps. Specific offerings feature various models of stainless steel magnetic driven centrifugal pumps (RMD, RMI, RML, RMW), fluorine-lined magnetic driven centrifugal pumps (RMD, RMI), self-priming fluorine-lined magnetic pumps (RMZ), and high-temperature magnetic pumps. These products are engineered for handling corrosive, environmentally hazardous, or difficult-to-process fluid media across diverse sectors such as petroleum, chemical, pharmaceutical, and new energy. Ricite operates a comprehensive factory with production, precision machining, assembly, and testing centers. The company holds multiple certifications including ISO 9001, ISO 14001, and ISO 45001, alongside various high-tech enterprise and credit ratings. Leveraging 30 years of experience from its parent company, Bainuo, Ricite emphasizes product reliability, energy efficiency, and environmental compliance. The company serves a worldwide market, with 40% to 50% of its products exported to North America, South America, Europe, Asia, the Middle East, Africa, and Oceania.
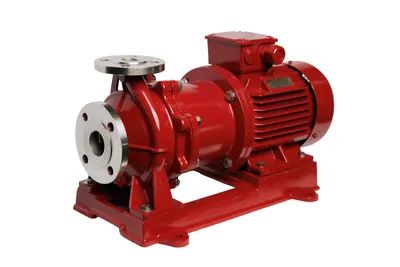
Stainless Mag-Drive Centrifugal Pump
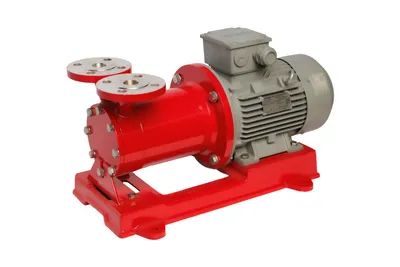
Mag-Drive Centrifugal Pump
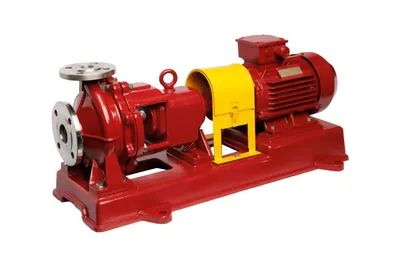
Horizontal Stainless Mag-Drive Centrifugal Pump
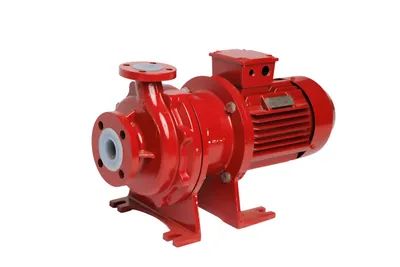
High Corrosion Resistance PFA-Lined Mag-Drive Centrifugal Pump
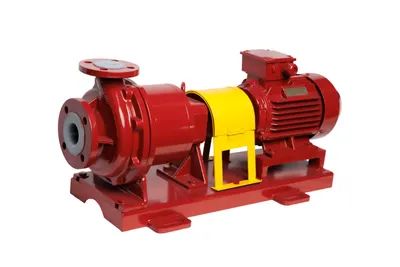
PFA-Lined Mag-Drive Centrifugal Pump
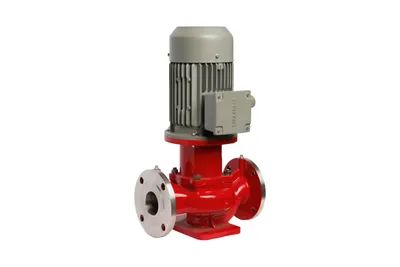
Vertical Stainless Mag-Drive Centrifugal Pump