Cixi Lanbao Electrical Co., Ltd.
Similar suppliers you may like
Ningbo Lanbao Electric Appliance Co., Ltd
🇨🇳 China
1993501-1000 peopleManufacturerHigh capacity factory
Established brand
OEM manufacturer
Description
Ningbo Lanbao Electric Appliance Co., Ltd is a professional manufacturer based in Ningbo, China, specializing in electrical and automotive accessories. Established in 1993, the company operates an 18,000 square meter factory and employs between 501 and 1,000 people. Their extensive product portfolio includes jump starters, battery chargers, power stations, cord reels, extension cords, and various lighting solutions such as LED and incandescent trouble lights. They also produce vacuum cleaners and thermoplastic-insulated wires.
The company is committed to high-quality standards and efficient operations, utilizing an ERP system to manage production and logistics. Their manufacturing capabilities are supported by a strict quality control system, evidenced by ISO 9001 certification. Furthermore, their products meet rigorous international safety and quality benchmarks, holding certifications such as UL, ETL, GS, CE, VDE, and EMC. Strategically located near major transport hubs like the Ningbo port and international airport, the company is well-positioned for international trade and timely global distribution.
Power Station (BFP-DA)
Cord Winder (AD-600)
Jump Start (BFP-A-1-WO)
LED Round Light (LED2)
LED Light (LED1)
Conductor Thermoplastic-Insulated Wire (1001/1401/1601/2426)
Incandescent Trouble Light (BFE-100)
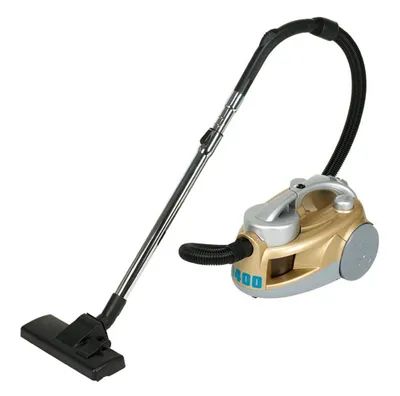
Vacuum Cleaner (AD006E)

Cixi Lanbo Electrical Appliance
🇨🇳 China
2002201-300 peopleManufacturer/Trading CompanyEstablished brand
OEM manufacturer
ODM manufacturer
Product customization
Shipments
38
Key market
North America
Description
Cixi Lanbo Electrical Appliance, also operating as Cixi Lotek Electrical Appliance, is a modernized high-tech manufacturer and exporter established in 2002. Based in Cixi, China, the company operates a 10,000-square-meter facility with comprehensive in-house capabilities, including design, pressing, printing, assembly, and testing. The enterprise specializes in two primary divisions: industrial heating solutions and small kitchen appliances. Its industrial portfolio features fan heaters (electric, diesel, kerosene, and LPG), infrared heaters, and industrial fans. The kitchen appliance division focuses on hand blenders, mixers, mini choppers, toasters, and coffee grinders. With an annual production capacity exceeding 800,000 units and annual revenues reaching up to USD 100 million, the company maintains a strong international presence across Europe, North America, the Middle East, and Southeast Asia. Cixi Lanbo is ISO 9001 certified and its products meet rigorous global standards, holding CE, GS, ETL, RoHS, and EMC certifications. The company offers flexible business models including OEM, ODM, and buyer label services, supported by a dedicated R&D team and advanced laboratory facilities.
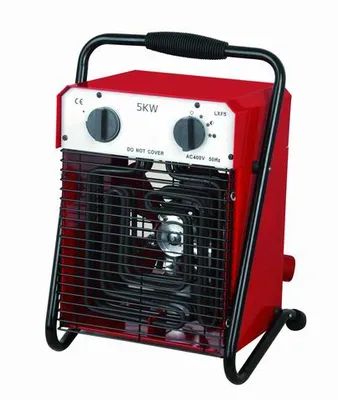
Industrial Fan Heater 5000W
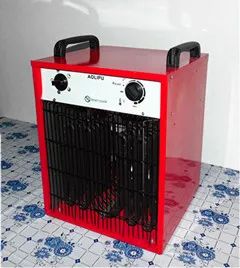
Industrial Heater 9kw
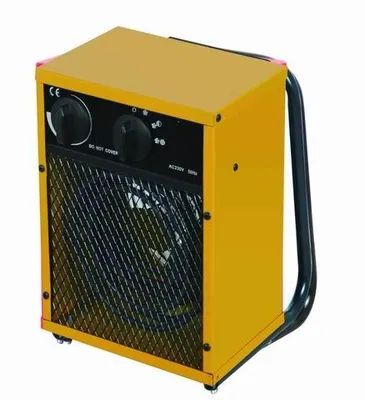
Industrial Fan Heater
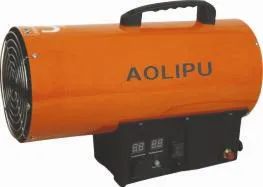
LPG/Gas Heater 10kw
50kw Industrial Gas Fan Heater
Gas Forced Air Heater (50KW)
15kw Industrial LPG/Propane Gas Hot Air Heater
Industrial Kerosene Heater (D030)$100
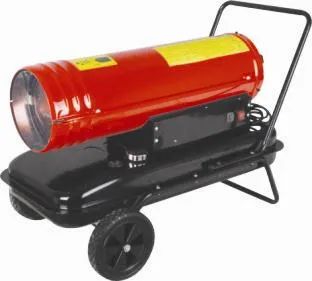
Diesel Air Heater (50KW)
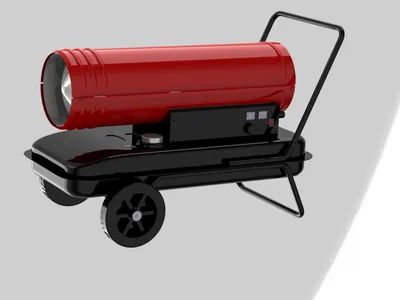
New Model for The Diesel Air Heater (D030)
Industrial Heater 3kw (RE003A)$15
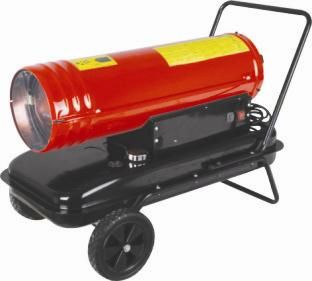
30kw Kerosene Heater$130


