Foshan Zhongxing Packaging Machinery Co., Ltd.
Similar suppliers you may like

Foshan Xinxing Machine Co.,Ltd.
🇨🇳 China
2003201-300 peopleManufacturer/Trading CompanyEstablished brand
High-tech enterprise
Own brand
Multi-country export
Shipments
155
Key customer
SUN PAPER SOURCE
Key market
🇮🇩 Indonesia
Description
Foshan Xinxing Machine Co.,Ltd. is a high-tech enterprise established in 2003, operating as both a manufacturer and trading company based in Foshan, China. With 201-300 employees, the company specializes in the R&D, production, and sale of packaging machinery, holding ISO 9001 certification. They offer a wide range of packaging solutions, including pillow type food packing machines, vertical packing machines, pre-made bag packing machines, and various paper and tissue packing machines such as facial tissue packaging machines, toilet roll bundle packaging machines, handkerchief packing machines, and sealing and cutting machines. Their product lines cater to diverse industries including baking, household paper, salt, medicine & dairy, quick-freezing, and leisure food. Foshan Xinxing Machine Co.,Ltd. emphasizes stringent quality control and continuous innovation, exporting its products to international markets across Southeast Asia, South America, Central America, East Europe, West Europe, and other regions.
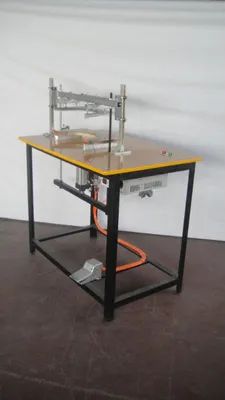
Small Cap Paper Sealing and Cutting Machine
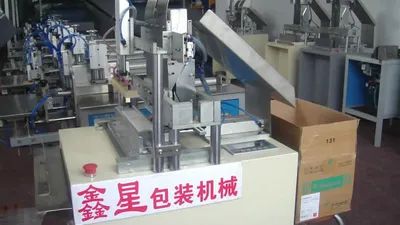
Semi-Auto Middle Bag Handkerchief Tissue Paper Packing Machine (822KC)

Foshan Zhongqi Packing Machinery Co., Ltd.
🇨🇳 China
200851-100 peopleManufacturer/Trading CompanyODM manufacturer
Low MOQ
Shipments
1
Key customer
IRINGA FOODS AND LOGISTICS
Key market
🇺🇸 United States
Description
Foshan Zhongqi Packing Machinery Co., Ltd. is a professional manufacturer and trading company established in 2008, specializing in the design, development, and production of automated packaging solutions. Based in Foshan City, Guangdong Province, the company operates a well-equipped factory and employs between 51 and 100 people. Their core product portfolio includes Vertical Form Fill Seal (VFFS) machines, sealing machines, filling machines, and specialized equipment for frozen fruits, vegetables, and snacks. They also provide semi-automatic packaging machines and roll film materials. With an annual sales figure exceeding US$3,000,000, the company maintains a strong international presence, exporting approximately 80% of its production to global markets including the United States, Brazil, Russia, UAE, and Iraq. All products are manufactured to comply with international quality standards, supported by comprehensive quality control throughout all production stages to ensure customer satisfaction.
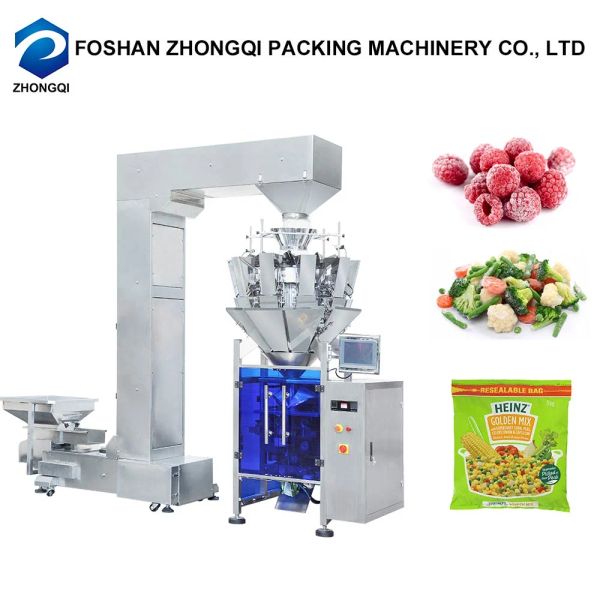
Frozen Fruit and Vegetable Packing Machine$12580
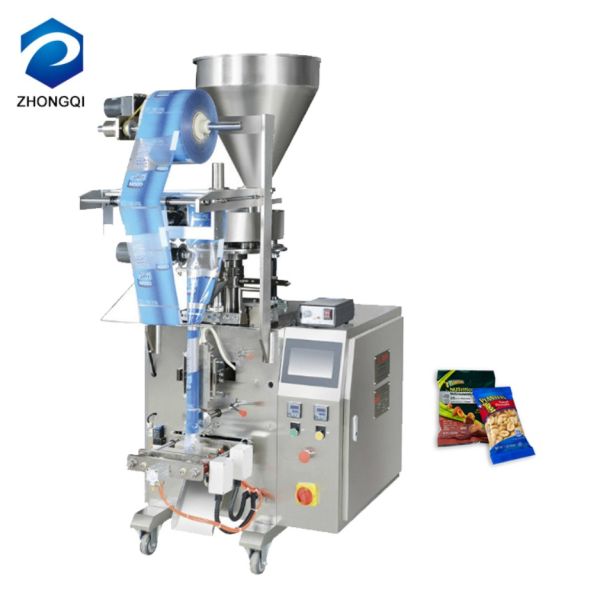
Semi-Auto Packaging Machine Snack Packing Machine$3800


