Guangdong Konix Technology Co., Ltd.
Similar suppliers you may like
Kingnix Technology Co., Ltd.
🇨🇳 China
51-100 peopleTrading Company/ManufacturerOEM manufacturer
High-tech enterprise
Description
Kingnix Technology Co., Ltd. is a Shenzhen, China-based company operating as both a manufacturer and trading company in the digital audio and video gadgets field. Established with an efficient R&D team and professional technical support, the company specializes in a range of consumer electronics. Their product portfolio includes MP3 players, MP4 players, and Digital Photo Frames, with a notable offering being a water-proof MP3 player. Kingnix Technology employs between 51 and 100 people and emphasizes strict quality control and a customer-centric approach to provide competitive gadgets.
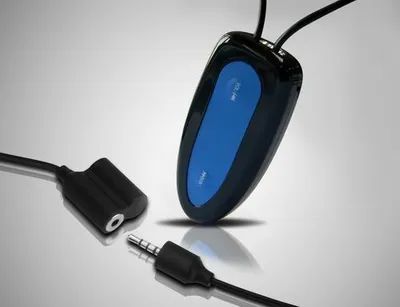
Water-Proof MP3 Player (KN98D)
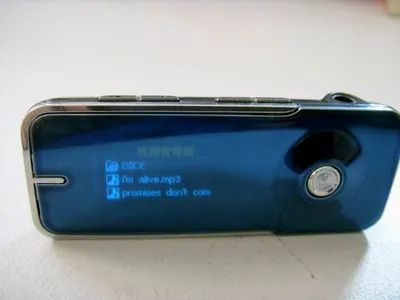
MP3 (KN01)
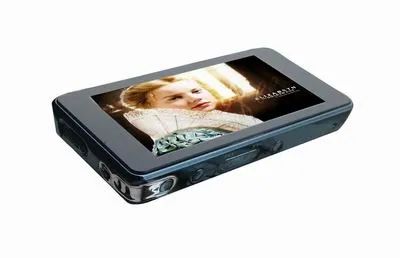
MP4 Player (KN502)
MP4 Player (KN506)
MP4 Player (KN069E)
MP4 Player (KN128)
MP4 Player (KN127)
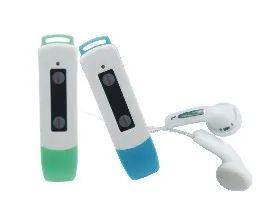
MP3 Player (KN93)
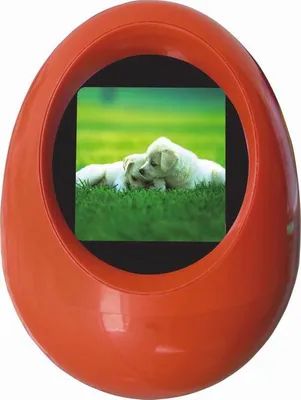
Digital Photo Frame (KPT15F)
Shenzhen Konx Smart Technology Co., Ltd.
🇨🇳 China
200951-100 peopleManufacturerOEM manufacturer
ODM manufacturer
Product customization
High-tech enterprise
Key market
Asia
Description
Shenzhen Konx Smart Technology Co., Ltd. is a professional manufacturer specializing in advanced security and wireless communication solutions. Established in 2009 and headquartered in Shenzhen, the company operates as an integrated enterprise encompassing R&D, production, and global sales. With a workforce of approximately 51 to 100 employees and a dedicated team of 30 development engineers, the firm focuses on delivering high-quality security surveillance products including smart doorbells, wireless video door phones, and digital peephole viewers.
The company is recognized for its innovation in wireless technology, offering a diverse product portfolio that features Tuya-integrated smart doorbells, fingerprint locks, E-locks, and portable fans. Their security solutions often incorporate high-definition 1080p cameras, night vision, and compatibility with smart home ecosystems like Alexa and Google Home. As an OEM and ODM service provider, Shenzhen Konx Smart Technology Co., Ltd. offers comprehensive solutions covering hardware, software, and system design tailored to specific client requirements.
Operating with a robust quality control system, the company has achieved ISO 9001 certification and ensures its products meet international standards such as CE, FCC, and RoHS. Their manufacturing capabilities are supported by advanced production equipment and a world-leading development laboratory. The company maintains a strong international presence, exporting its products to diverse markets across North America, Europe, Asia, Africa, and Australia.
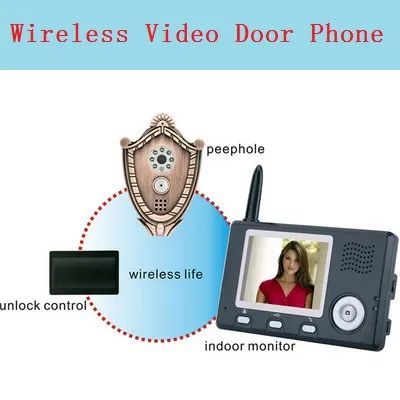
Wireless Video Peephole Viewer (PH3501)


