Material Flow & Conveyor Systems, Inc.
Similar suppliers you may like
Taylor Material Handling & Conveyor
🇺🇸 United States
194011-50 peopleManufacturer/Distributor/Service CompanyEstablished brand
OEM manufacturer
Product customization
Industry association member
Key customer
ADVANCED CONVEYOR SYSTEMS
Key market
🇺🇸 United States
Description
Taylor Material Handling & Conveyor (TMHC) is a premier turnkey systems integrator, custom manufacturer, and distributor based in Toledo, Ohio. With a legacy spanning over 50 years, the company provides comprehensive material handling and conveyor solutions to a diverse range of industries, including automotive, food and beverage, pharmaceuticals, glass, and general manufacturing. TMHC serves as a single-source provider for OEMs and small manufacturers, offering end-to-end services that encompass design, engineering, custom fabrication, electrical control system programming, and field installation.
The company specializes in an extensive array of conveyor systems, including 24 VDC powered roller, accumulation, sanitary, magnetic, and overhead conveyors. Beyond conveying, their portfolio features ergonomic lifting solutions, overhead cranes, vacuum lifting equipment, industrial racking, and production packaging machinery such as case erectors and stretch wrappers. As a contract manufacturer, TMHC operates a factory equipped for steel fabrication, machining, and the assembly of custom equipment like robotic palletizing lines and powered transfer tables.
In addition to its manufacturing capabilities, TMHC is an authorized distributor for leading brands such as Modular Conveyor Express (MCE), Hytrol, Gorbel, and Anver. The company provides critical support services including equipment refurbishing, PLC programming, and safety inspections. Serving clients across the United States—with a strong regional presence in Ohio, Michigan, Indiana, and Pennsylvania—Taylor Material Handling & Conveyor is dedicated to enhancing industrial productivity through automated and custom-engineered material handling systems.
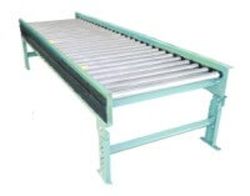
24 VDC Conveyors – 196 PR Series

Fluent Conveyors
🇺🇸 United States
201511-50 peopleManufacturer/Service CompanyProduct customization
Industry association member
OEM manufacturer
Key customer
ANHEUSER BUSCH
Key market
🇺🇸 United States
Description
Fluent Conveyors, founded in 2015 and based in Denver, Colorado, is a US-based manufacturer and service company specializing in custom conveyor systems and replacement parts. With 11-50 employees and an annual revenue of $4.6 million, the company operates through a strong dealer network across the United States, Canada, and Mexico. Fluent Conveyors offers a comprehensive range of conveyor solutions, including heavy-duty and light-duty roller chain conveyors, slider bed conveyors, trough idler conveyors, and various recycling sort systems. They also provide a full suite of replacement parts such as shafts, motors, pulleys, idlers, sprockets, and bearings, along with diverse replacement conveyor belts. Emphasizing high-end workmanship and bespoke material handling systems, Fluent Conveyors utilizes laser precision and the latest technology in their manufacturing processes. They offer OEM and ODM services, with products designed for industries including Bio-Fuel, Carpet Recycling & Processing, Construction & Demolition, OCC Recycling, Package Handling, and Waste Management. The company holds UL certifications and focuses on continuous innovation and customer satisfaction, providing pre-sales consultation and engineering services.