Shandong Zhongkun Lanyuan Environmental Engineering Co., Ltd.
Similar suppliers you may like

Shandong Yongkun Environmental Protection Equipment Co., Ltd.
🇨🇳 China
202311-50 peopleManufacturerIndustry association member
High-tech enterprise
Low MOQ
Description
Shandong Yongkun Environmental Protection Equipment Co., Ltd. is a contract manufacturer based in Zibo, China, specializing in comprehensive environmental protection solutions. Established in 2023, the company operates a factory covering 20 mu and employs 11 to 50 people. They are a core technology enterprise in China's environmental protection industry and a member of the National Water Treatment Association. Shandong Yongkun Environmental Protection Equipment Co., Ltd. provides solutions for organic waste gas, organic wastewater, membrane separation, and ion exchange products. Their extensive product range includes water treatment equipment such as quartz sand filters, activated carbon filters, multi-media filters, manganese sand filters, iron removal filters, integrated water purifiers, ultrafiltration equipment, reverse osmosis equipment, and nanofiltration equipment. They also offer various ion exchangers (sodium, anion, cation, mixed), sewage equipment, waste gas adsorption equipment, ventilation equipment, dust removal equipment, denitrification equipment, pharmaceutical equipment, pipeline valves, and anti-corrosion equipment, including PTFE, plastic, and rubber linings. With a highly skilled technical team possessing over 20 years of practical experience, the company serves diverse industries including chemical, food, medicine, electricity, oil, paper, printing and dyeing, electronic metallurgy, and smelting. Shandong Yongkun Environmental Protection Equipment Co., Ltd. is ISO 9001 certified, ensuring high-quality products and services.
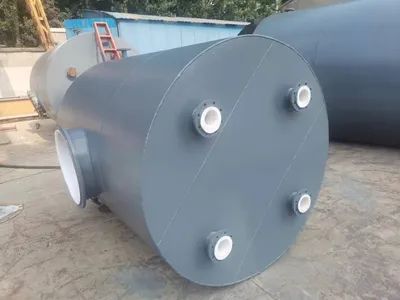
Rubber Equipment Plastic Equipment PTFE Equipment
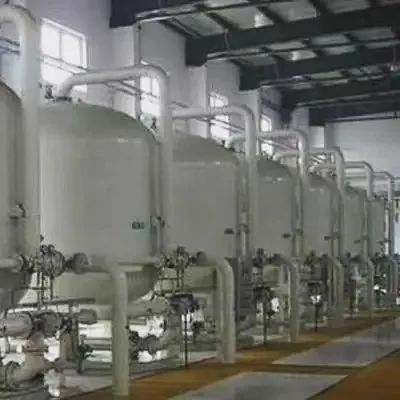
Multi-Media Filter
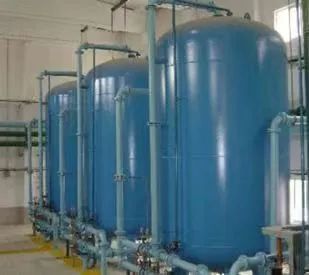
Mixed Ion Exchanger
Shandong Zhongxin Environmental Engineering Co., Ltd
🇨🇳 China
101-200 peopleManufacturer/Trading CompanyHigh-tech enterprise
Low MOQ
Description
Shandong Zhongxin Environmental Engineering Co., Ltd is a high-tech enterprise and a key environmental protection enterprise of Shandong province, operating as both a manufacturer and trading company. Established as a subsidiary of Haihui Group, the company was organized by Tsinghua University, Tianjin University, and Qingdao University, combined with the Shandong Academy of Environmental Science. With 101 to 200 employees, including approximately 140 professional technical staff with over one-third being senior specialists, the company focuses on "Science Advanced, Technology Developed" and "For Customer, For Public" principles. They specialize in industrial equipment and components, and manufacturing and processing machinery, with a focus on environmental protection. Their main products include bag filters, belt conveyors, idlers, conveying machinery, dust removal equipment, and sewage treatment equipment. The company offers contract manufacturing services and has established a standardized modern enterprise system driven by innovation.
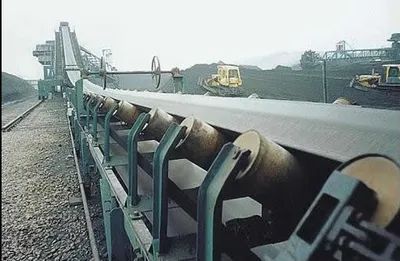
Belt Conveyor
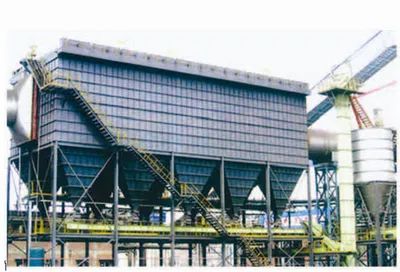
Bag Filter
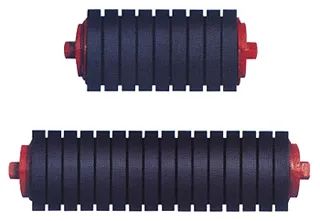
Buffer Roller
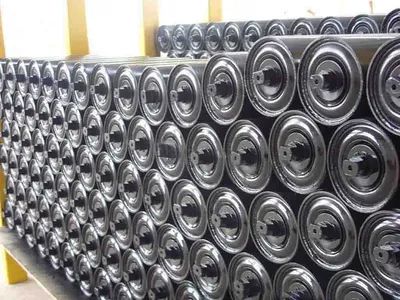
Idlers
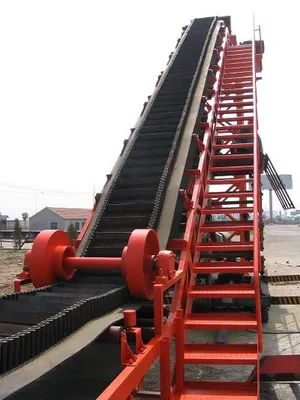
Large Inclination Belt Conveyor


