Shenzhen Best-Friends Silicone Rubber Products Factory
Similar suppliers you may like
Shenzhen Best Silicone Products Co., Ltd.
🇨🇳 China
200311-50 peopleManufacturerEstablished brand
OEM manufacturer
ODM manufacturer
Product customization
Key market
🇺🇸 United States
Description
Shenzhen Best Silicone Products Co., Ltd. is a professional manufacturer based in Shenzhen, China, specializing in the production of silicone rubber and PVC products for the global market. Established in 2003, the company operates a dedicated factory and employs between 11 and 50 people. They offer comprehensive OEM and ODM services, welcoming custom designs and specifications to meet diverse client needs. The company's extensive product portfolio spans multiple industries, including apparel accessories, household goods, and promotional gifts. Key offerings include silicone bracelets, keypads, labels, keychains, swimming caps, and non-slip pads. They also specialize in personal care and fashion items such as silicone bras, breast inserts, and nude sandals. Additionally, the company produces functional accessories like silicone cup covers, cable winders, HDD protectors, and silicone gloves. With nearly two decades of experience, Shenzhen Best Silicone Products Co., Ltd. has established a presence in international trade, with shipment records indicating exports to major North American ports such as Seattle and Los Angeles. The company is committed to providing high-quality products and competitive pricing across its diverse range of silicone and PVC solutions.
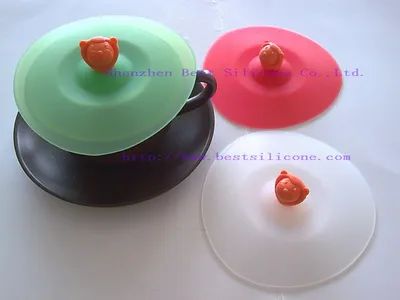
Silicone Cup Cover (MCC-013)
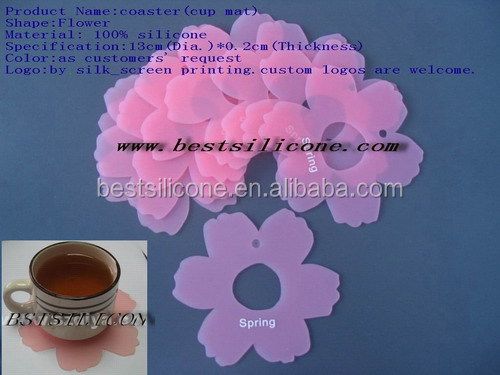
Oem Promotional coaster (CM-041)$0.3
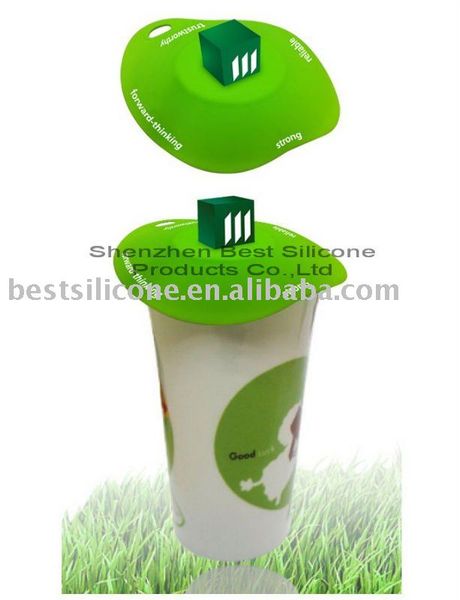
Promotion Gift Silicone Cup Cover$0.5
OEM Silicone case$0.08
Customized Soft PVC Label$0.81
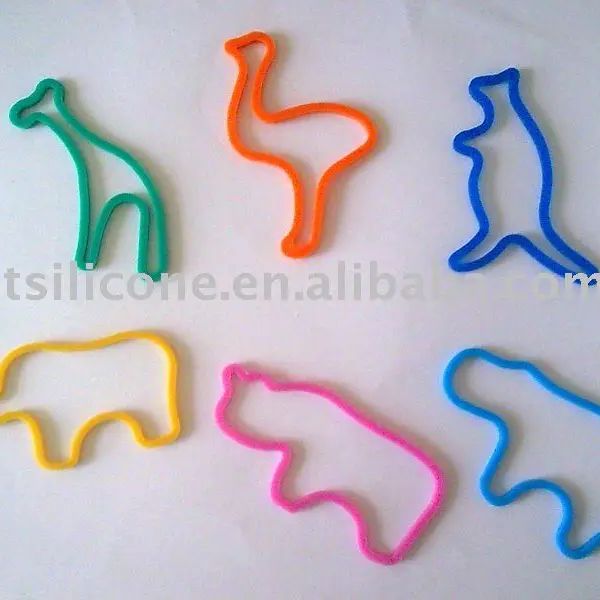
Ametabolic Silicone Animal Rubber Band-Zoo(SAB-002)$0.75
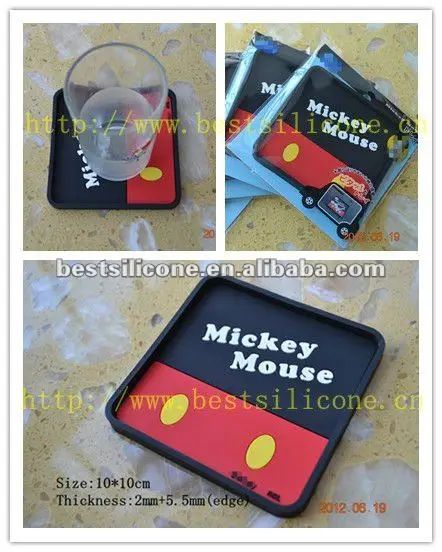
Soft PVC coaster (CM-042)$0.3
Best Silicone Rubber Co., Ltd
🇨🇳 China
198351-100 peopleManufacturer/Trading CompanyEstablished brand
OEM manufacturer
ODM manufacturer
Key market
Europe
Description
Best Silicone Rubber Co., Ltd is a professional manufacturer and trading company specializing in high-quality silicone products for industrial and consumer markets. Established in 1983 with operations in Hong Kong and a factory in Shenzhen, China, the company provides comprehensive one-stop solutions including design, engineering, and manufacturing. They operate as a leading ODM and OEM partner, employing between 51 and 100 people with a dedicated R&D team focused on product innovation. Their extensive manufacturing capabilities cover industrial components such as silicone rubber keypads, membrane switches, gaskets, and zebra connectors, as well as consumer goods including kitchenware, medical accessories, and promotional gifts. The company maintains a strong international presence, exporting over 90% of its production to global markets. Their commitment to quality is demonstrated through state-of-the-art machinery and compliance with international standards, including RoHS, FDA, CPSIA, and EN71 certifications. With an annual output value reaching up to US$100 million, they serve diverse industries ranging from electronics and healthcare to household commodities.
Oem Promotional coaster (CM-041)$0.3
Promotion Gift Silicone Cup Cover$0.5
OEM Silicone case$0.08
Customized Soft PVC Label$0.81
Ametabolic Silicone Animal Rubber Band-Zoo(SAB-002)$0.75
Soft PVC coaster (CM-042)$0.3


