Tianjin First Cold Chain Equipment Tech Co., Ltd.
Similar suppliers you may like
Tianjin Junrui Refrigeration Equipment Co., Ltd.
🇨🇳 China
19705-10 peopleManufacturerEstablished brand
ODM manufacturer
Own brand
Low MOQ
Shipments
1
Key customer
DEVEX
Key market
Europe
Description
Tianjin Junrui Refrigeration Equipment Co., Ltd., also known as Tianjin Hongqi Refrigeration Equipment Co., Ltd., is a contract manufacturer of refrigeration equipment based in Tianjin, China. Established in 1979, the company has nearly 40 years of experience in designing, manufacturing, installing, and maintaining refrigeration equipment. Operating a factory spanning over 30,000 square meters in the ZhongBei industrial park, Tianjin Junrui Refrigeration Equipment Co., Ltd. utilizes advanced production lines, including German-imported high-pressure foaming machines, for the production of polyurethane sandwich panels. The company specializes in cold storage solutions, offering a comprehensive range of products such as cold storage panels, various types of cold room doors (including automatic sliding and hinged doors), polyurethane freezer panels, and specialized refrigeration units like ice machines, flake ice machines, fresh milk preservation cabinets, spiral evaporators, serpentine evaporators, and cadaver cold storage cabinets. Their "RuiBing" brand polyurethane sandwich panels and doors are widely used in food production, quick-frozen food processing, aquatic product processing, crop storage, pharmaceuticals, purification, and logistics centers. The company holds a National Industrial Product Production License and has been recognized as a recommended product for China's refrigeration and air conditioning equipment. Tianjin Junrui Refrigeration Equipment Co., Ltd. exports its products to numerous countries, including Japan, Thailand, Korea, the Philippines, Australia, Israel, Canada, South Africa, and the United States.
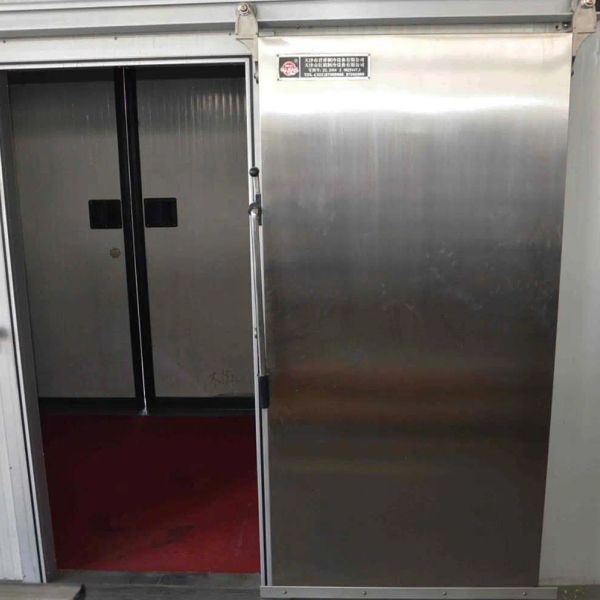
Cold Storage/Room Door, Made in China Good Quality Cold Room Door$10
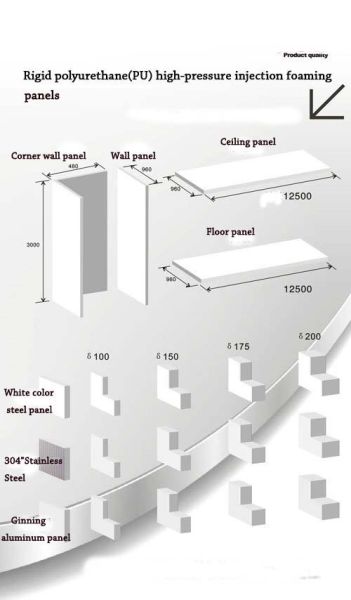
75mm/100mm/120mm/150mm/200mm Polyurethane Freezer PU Cold Room Panel$10
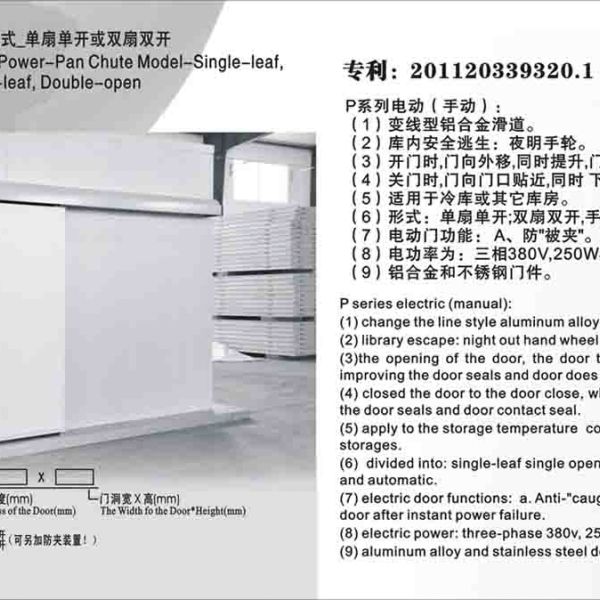
Automatic Cold Room Sliding Doors, Refrigerator Doors$10
Tianjin Yulian Cold Chain Technology Co., Ltd.
🇨🇳 China
201011-50 peopleManufacturerHigh-tech enterprise
ODM manufacturer
Description
Tianjin Yulian Cold Chain Technology Co., Ltd. is a high-tech manufacturer based in Tianjin, China, specializing in the design and production of advanced cold chain materials for the transport industry. Established between 2008 and 2010, the company employs a dedicated team of 11 to 50 professionals. They are recognized for integrating European cold chain technology and design principles into their manufacturing processes, positioning themselves as a unique provider of complete cold box sets specifically engineered for the pharmaceutical and biological sectors. Their specialized medicine cold boxes utilize multilayer macromolecular heat preservation materials, offering high performance with up to 120 hours of cold retention while remaining lightweight for easy transport. Beyond medical applications, the company offers a diverse product portfolio including automotive and fishing cold boxes, daily use ice storage boxes, medicine cold bags, insulation packages, and gas collection bags. Their expertise spans across the manufacturing of cases, boxes, and specialized chemical cooling materials such as ice packs.
Medicine Cold Box
Ice Pack
Medicine Ice Box
Daily Cold Box
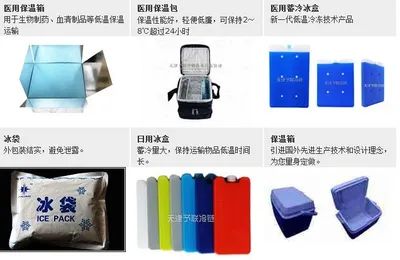
Specialized Case


