Xinxiang Mingyan Screening Machinery Co., Ltd.
Similar suppliers you may like
Xinxiang Mingyang Sieving Machinery Co., Ltd.
🇨🇳 China
2010101-200 peopleManufacturer/Trading Company/DistributorOEM manufacturer
Low MOQ
Patented technology
High-tech enterprise
Key market
North America
Description
Xinxiang Mingyang Sieving Machinery Co., Ltd. is a professional manufacturer and trading company established in 2010, specializing in fine material screening and material handling equipment. Based in Xinxiang City, Henan Province, the company operates from an 8,000-square-meter modern production facility and employs between 101 and 200 personnel, including a dedicated team of 20 technicians and R&D staff. The company is ISO 9001 and ISO 14001 certified, emphasizing quality control and scientific innovation through collaborations with research institutions and universities.
Their extensive product portfolio focuses on accurate material classification and includes Rotary, Ultrasonic, and Linear Vibrating Screens, as well as Test Sieves, Drum Screens, and High-Frequency Screening Machines. Beyond sieving, the company provides comprehensive industrial solutions such as bucket elevators, screw conveyors, belt conveyors, and various mixing equipment including horizontal spiral ribbon mixers and double-spiral conical mixers. These products serve diverse sectors, including the chemical, pharmaceutical, food, and metallurgical industries.
As an OEM and contract manufacturer, Xinxiang Mingyang Sieving Machinery Co., Ltd. possesses independent intellectual property rights and utilizes advanced mechanical design and computerized simulation test systems. The company maintains a strong international presence, exporting to markets across North America, South America, and Eastern Europe, with annual revenues estimated between US$1 Million and US$10 Million.
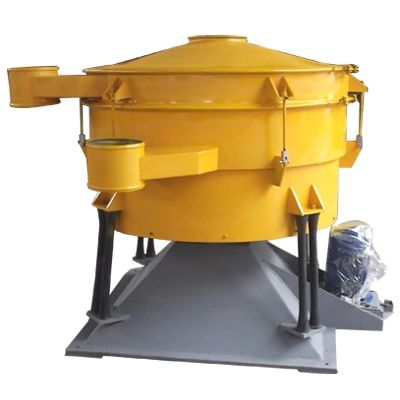
Tumbler Screening Separator Made in Mingyang$1667
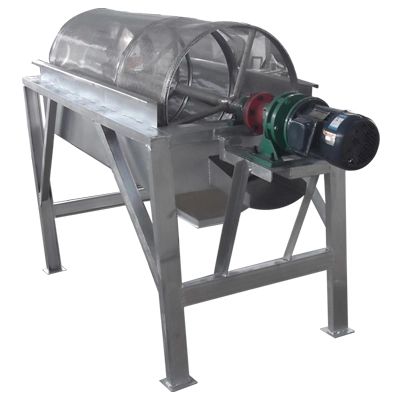
Mingyang Trommel Vibrating Screen$835
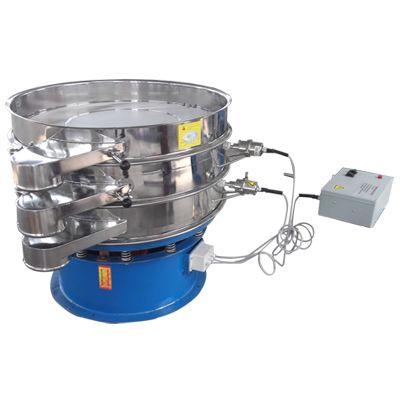
Ultrasonic Vibrating Screen for Powder, Particle Made in China$2500
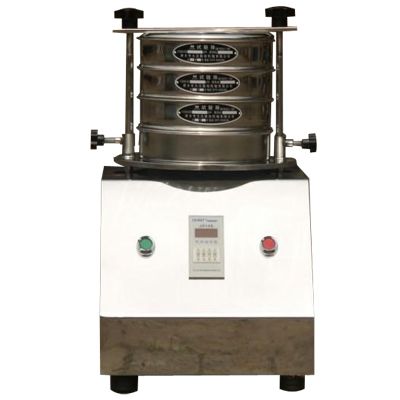
Standard Testing Sieve, Screening Machine, for Powder, Particle$600
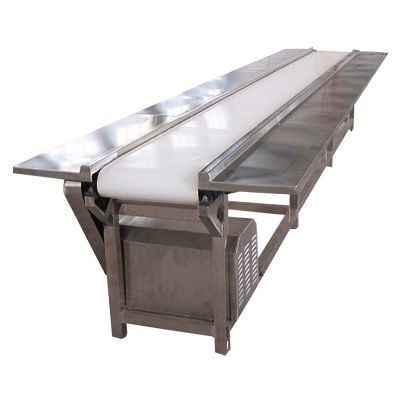
Stainless Steel Belt Conveyor, Belt Conveyor for Food Industry$1827
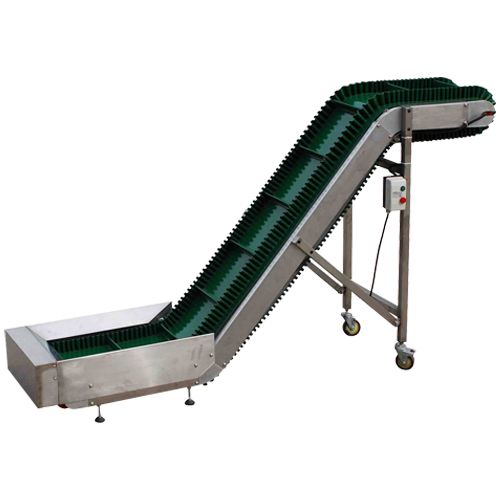
Large Angle Belt Conveyor for Rice Made in China$656
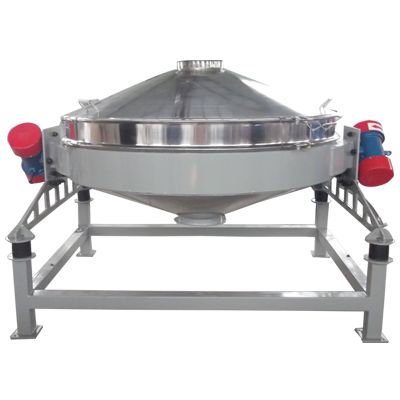
Vertical Discharge Vibrating Screen, Vibrating Sieve Made in China$2556
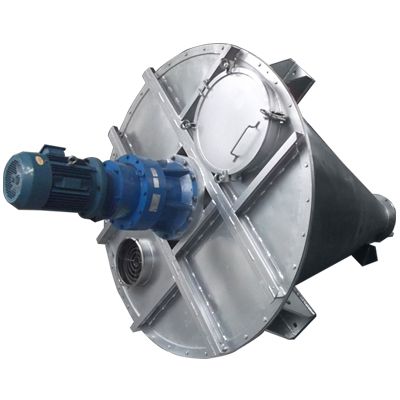
Double-Spiral Conical Mixer for Powder and Particle Made in China$5000
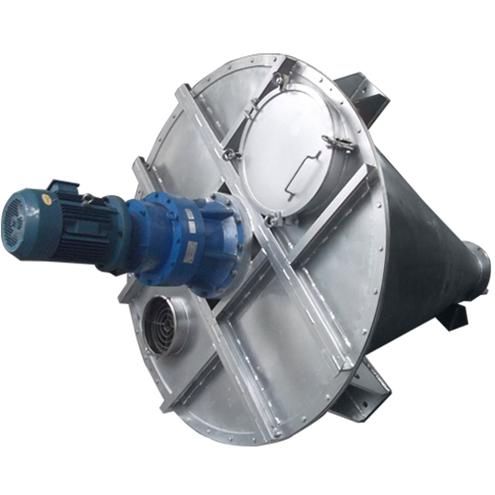
Double-Spiral Conical Mixer for Powder and Particle$1500
Foldable Climbing Belt Conveyor System for Material Handling
High Efficiency, Low Price Heavy Vibrating Screen,henan Zsg High Efficiency Heavy Mining Vibratin

Mega Young Screening Technology Co., Ltd.
🇨🇳 China
2017201-300 peopleManufacturer/Trading CompanyOwn brand
Product customization
ODM manufacturer
OEM manufacturer
Shipments
34
Key customer
TERMOLITA
Key market
South America
Description
Mega Young Screening Technology Co., Ltd. is a professional manufacturer and trading company headquartered in Xinxiang, China, specializing in the research, development, and production of industrial screening and conveying equipment. Established in 2010, the company operates a large-scale manufacturing facility with over 10 production lines and a workforce of 201 to 300 employees. They are recognized for their expertise in OEM and ODM services, providing customized material handling solutions for global clients in the chemical, mineral, food, agriculture, and recycling industries.
The company's core product portfolio centers on advanced gyratory screening technology, including the M&Y series gyratory screeners, lateral structure gyratory sifters, and side-door access models designed for high-capacity precision and easy maintenance. Their technical capabilities extend to a wide range of separation machinery such as vibrating screens, tumbler screeners, and fine screening machines. Complementing their screening line, Mega Young produces robust conveying systems, including screw, belt, and chain conveyors, as well as vibrating feeders.
With an annual output value between US$10 million and US$50 million, Mega Young Screening Technology serves a prestigious international clientele, including major organizations such as COFCO, Dow Chemical, and Armstrong. The company provides a comprehensive service package that encompasses on-site surveying, non-standard design, installation guidance, and 24-hour post-sales support. Their commitment to innovation is reflected in their specialized R&D efforts focused on reducing equipment downtime and improving screening efficiency for bulk solids and fine powders.
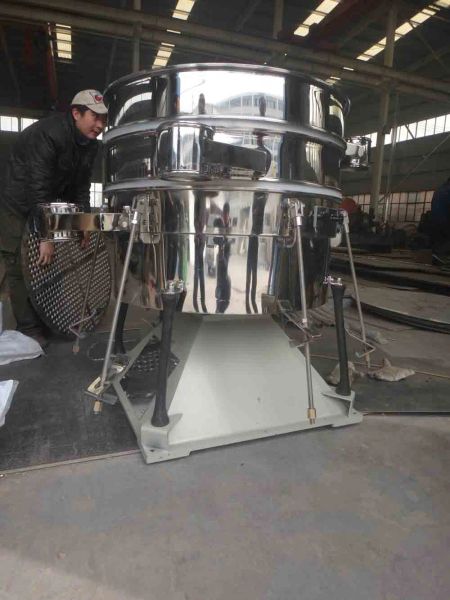
Tumbler Vibrating Screen$8000
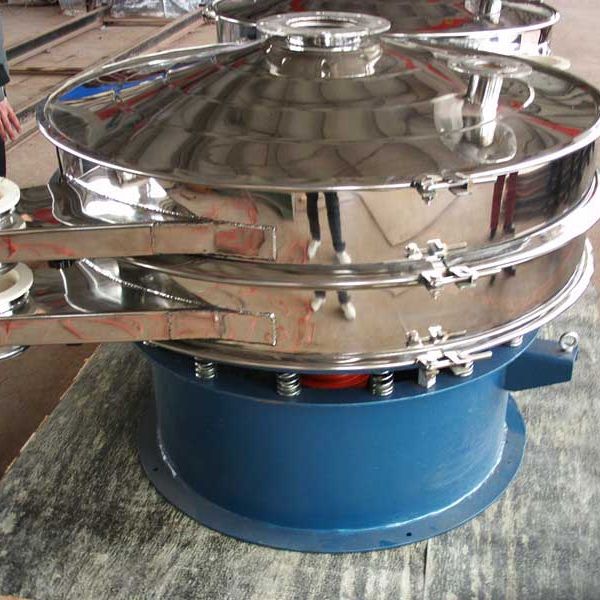
Round Vibrating Screen$4000
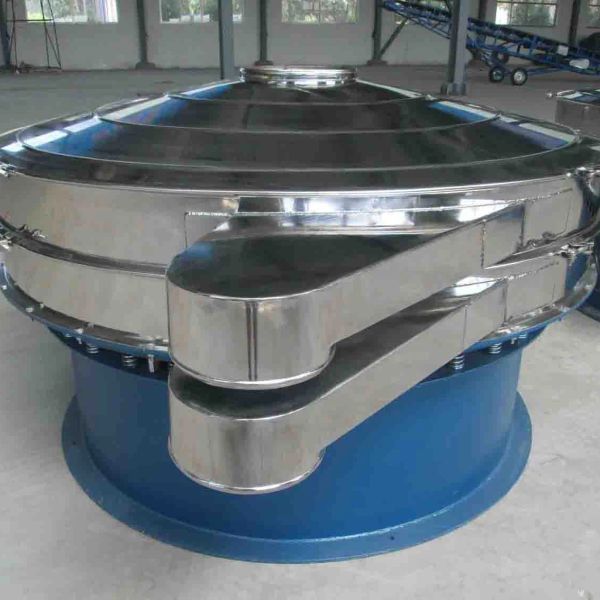
Round Vibro Sieve$4000


