Bio-Shine Inc.
Similar suppliers you may like
Bishine Technology
🇨🇳 China
1999501-1000 peopleManufacturerHigh capacity factory
Established brand
OEM manufacturer
ODM manufacturer
Key market
North America
Description
Bishine Technology is a high-tech manufacturer specializing in portable storage devices and digital products, established in 1999. Headquartered in Hong Kong with a factory base in Shenzhen, China, the company operates with 501-1000 employees and generates an annual turnover exceeding 6 million USD. Bishine Technology is a professional OEM/ODM contract manufacturer, offering services for products such as MP4 players, USB flash drives, digital photo frames, GPS devices, and solar chargers. The company maintains 10 product lines within its 3,000-5,000 square meter factory and adheres to systematic quality control and management processes based on ISO 9000/9001 standards. Their products are certified with CE, FCC, and RoHS. With a strong focus on R&D, including an in-house molding department for new designs, Bishine Technology exports 81-90% of its products to international markets including North America, South America, Europe, the Middle East, and Southeast Asia.
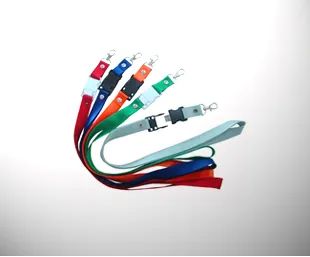
FLash Disk (USB35)
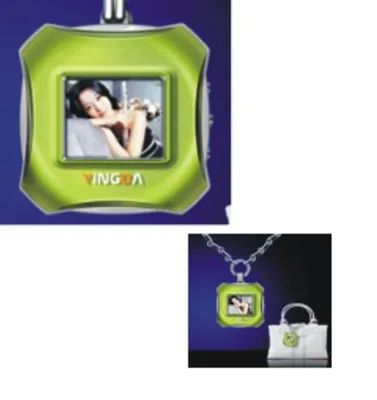
DPF (DF-A5)
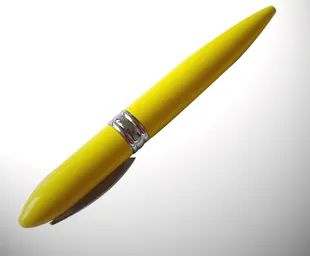
Pen Drive (UP04)
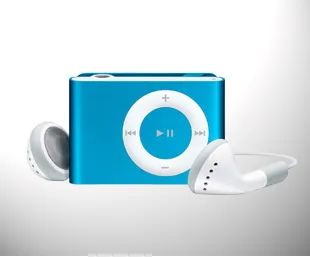
MP3 (2)
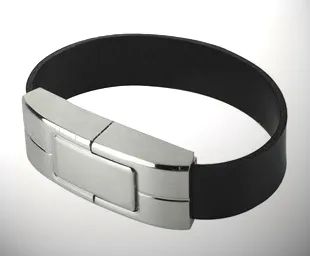
USB FLash Disk (USB26)
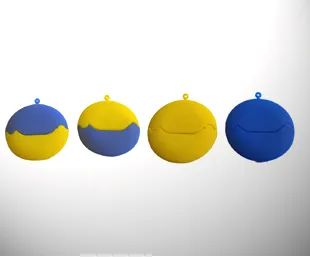
USB Disk (USB15)
Digital Photo Frame (DF-A)
GPS

E-Shine Antimicrobial
🇨🇳 China
201711-50 peopleTrading CompanyHigh-tech enterprise
Product customization
Key market
Asia
Description
E-Shine Antimicrobial is a specialized trading company and R&D-focused provider of antimicrobial solutions based in Xiamen, China. Founded in 2017, the company leverages over a decade of industry expertise and 14 years of international business experience to deliver innovative antimicrobial technologies. E-Shine Antimicrobial collaborates with prominent university laboratories to develop a diverse product portfolio that includes antimicrobial powders, solutions, plastic masterbatches, and specialized textiles such as polyester yarn, staple fibers, and nonwovens. Their product range features advanced silver ion and copper ion-based materials, as well as antimicrobial coatings, antimildew solutions, and deodorant powders. The company provides tailored OEM services and technical support to help clients across various industries integrate antimicrobial properties into their end products. With a focus on international standards, their solutions are utilized in markets across North America, Europe, and Asia, ensuring high-performance results that meet rigorous global testing requirements.
Copper-Based Antimicrobial Antibacterial Polyester Staple Fiber
Silver Ion Antibacterial Antimildew Antimite Polyester Staple Fiber
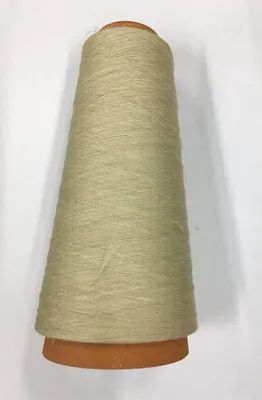
Copper Ion Based Antimicrobial Antibacterial Polyester Cotton Blended Yarn
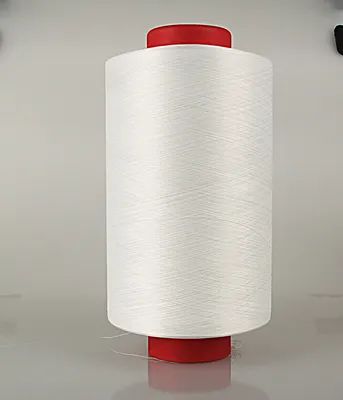
Silver Ion Antimicrobial Antimildew Antimite Polyester Yarn