Brownlee-Morrow Company
Brownlee-Morrow Company
🇺🇸 United States, Alabama
195251-100 peopleManufacturer/Distributor/Service CompanyBrownlee-Morrow Company is a family-owned manufacturer, distributor, and service provider specializing in fluid and air handling solutions. Established in 1952 and headquartered in Birmingham, Alabama, the company serves the Southeastern United States with additional locations in Mobile and Nashville. As a contract manufacturer and distributor, they provide a comprehensive range of industrial equipment, including centrifugal and positive displacement pumps, industrial fans, blowers, dust collectors, and mechanical seals. Their product portfolio also extends to process equipment such as flow meters, heat exchangers, and motor controls.
With a team of experienced engineers and technicians, Brownlee-Morrow Company offers custom fabrication, 3D modeling, and system design to meet unique customer requirements. They operate a dedicated factory and provide extensive field services, including equipment repair, laser alignment, and emergency support for rotating machinery. The company serves a diverse array of sectors, including municipal water, power generation, mining, automotive, chemical, pulp and paper, marine, and food and beverage industries. They are associated with a group of specialized companies including Morrow Repair Services and Vulcan Pumps, and they distribute products from leading brands such as Goulds, Viking, and Camfil.
OEM manufacturerOffers OEM services for customized brand manufacturing.
Product customizationOffers full customization for design and features.
Established brandFounded in 1952, with over 20 years of industry experience.
Contact
*******************
2
************
5
Products
Products
0
Categories
0
Air Pollution Control
0·0 reviews
Air Pollution Control
0·0 reviews
Air Handling/Control
0·0 reviews
Fans and Blowers
0·0 reviews
Fans and Blowers
0·0 reviews
Air Handling/Control
0·0 reviews
Customers
ABB
1
***
***
*************
***
Unlock all 31 customers
Ask AI about this supplier
Similar suppliers you may like

R.M. Headlee Co., Inc.
🇺🇸 United States
197011-50 peopleDistributor/Service CompanyEstablished brand
Industry association member
Shipments
53
Key customer
INGERSOLL RAND
Key market
🇮🇳 India
Description
R.M. Headlee Co., Inc. is a premier distributor and service provider specializing in industrial process valves, valve automation, and pressure management solutions. Founded in 1970 and headquartered in Orchard Park, New York, the company operates as a technical sales leader with a dedicated automation center and warehouse. They serve a diverse range of sectors, including Natural Gas, Industrial, Municipal, Power Generation, Water Distribution, and Research & Development. With a team of approximately 11 to 50 employees, the company provides comprehensive technical services such as evaluation, design, specification, and commissioning solutions.
The company maintains an extensive inventory of high-quality components, including butterfly, ball, check, knife gate, and automatic control valves, alongside pneumatic and electric actuators. Their product portfolio also encompasses pressure relief valves, rupture discs, expansion joints, steam products, and specialized systems for potable water mixing and aeration. R.M. Headlee Co., Inc. is an authorized distributor for numerous industry-leading manufacturers, including Pratt, Auma, Tideflex, Red Valve, Cla-Val, and Val-Matic, ensuring compliance with AIS/BABA standards where required.
Beyond product distribution, the company is a recognized educational resource, serving as an approved sponsor for continuing education for Professional Engineers and Plant Operator training in New York State. This commitment to technical expertise and customer requirements allows them to deliver sophisticated process piping solutions across the Northeastern United States, including New York, New Jersey, and Pennsylvania.
Pneumatic Accessories
Corrosion Products
Valve Automation
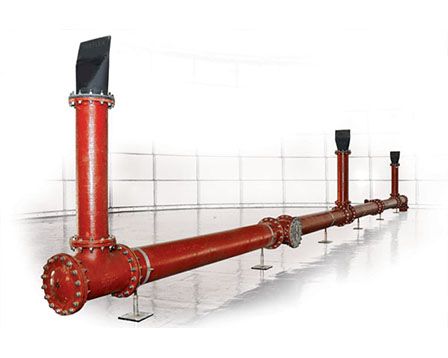
Potable Water Mixing Systems
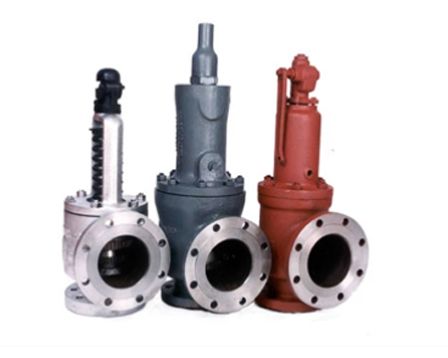
Pressure Management
Valve Actuators
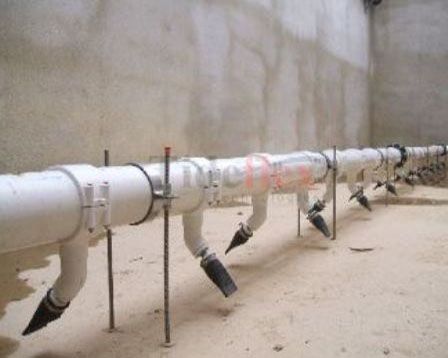
Aeration Systems
Valve Actuators
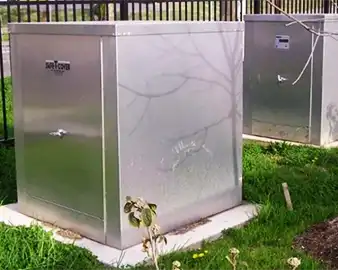
Aluminum Backflow Enclosures
Pneumatic Accessories
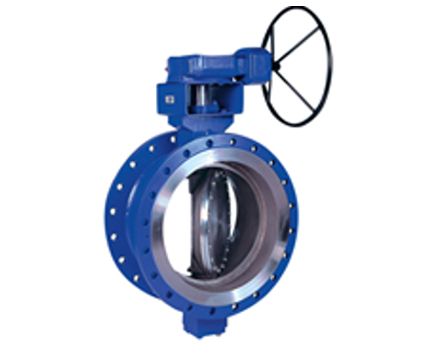
Valves
Potable Water Mixing Systems
Brown Tape Products Company
🇺🇸 United States
198411-50 peopleTrading Company/DistributorEstablished brand
Key customer
ASHLAND CHEMICAL CORPORATION
Key market
🇺🇸 United States
Description
Brown Tape Products Company is a specialized distributor and trading company headquartered in Indianapolis, Indiana. Incorporated in 1984, the company leverages over 40 years of industry expertise to provide high-quality industrial specialty adhesive tapes and packaging supplies. Operating with a team of 11 to 50 employees, they serve a diverse global clientele across the entertainment, manufacturing, automotive, and healthcare sectors, including major corporations such as Clear Channel Entertainment and Ashland Chemical Corporation. The company offers an extensive product portfolio that includes gaffers tape, spike tape, duct tape, vinyl tape, and water-activated tape. Their technical offerings feature specialized solutions such as high-temperature masking tape, aluminum foil glass cloth with silicone adhesive, and heavy-duty premium cloth duct tape designed for high-tensile applications. Other key categories include Mylar, polyester, pipe wrap, foam, and high-bond tapes, as well as double-coated polyester and vinyl electrical insulating tapes. Brown Tape Products Company focuses on personalized service, including stock monitoring and timely reorder management, to ensure reliable delivery and competitive pricing for its business partners.
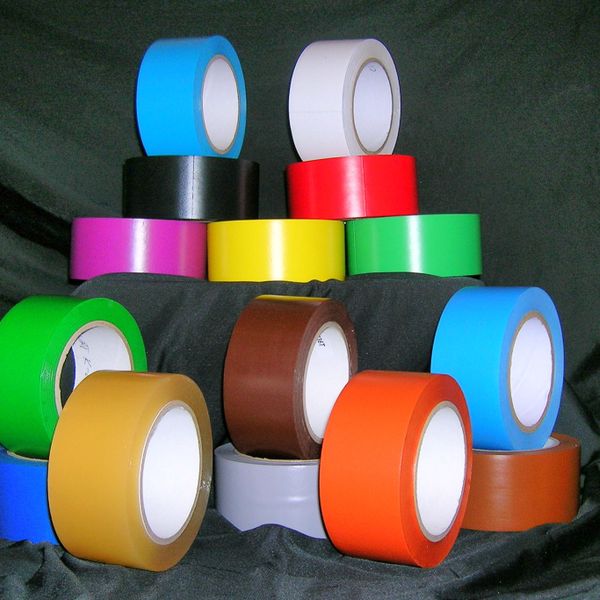
Colored Vinyl Tapes (matte surface-soft PVC). 3inch neutral core/carton.
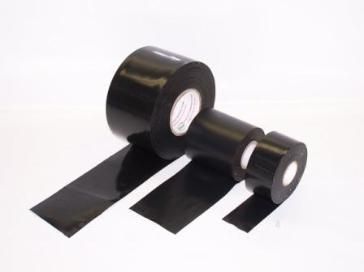
SPVC PIPE WRAP/Surface Protection Film
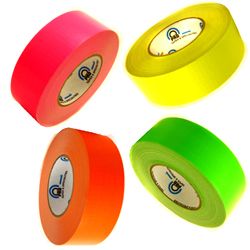
Fluorescent Gaffers/Spike Tape (mate finish)
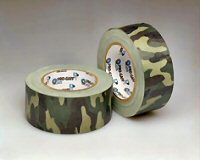
Camouflage Cloth Duct Tape
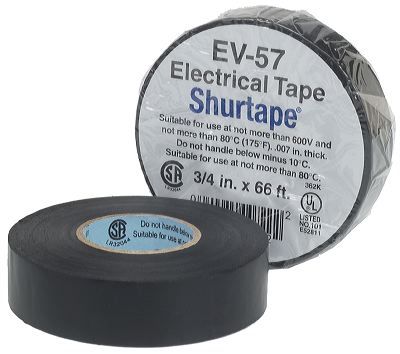
ALL Weather-Flame retardant and cold resistant
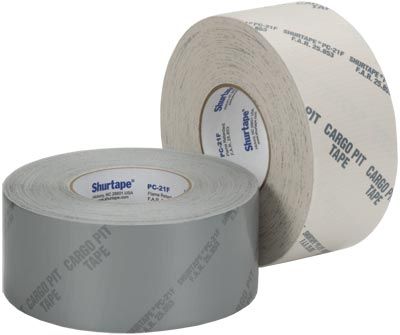
Flame retardant and cold resistant
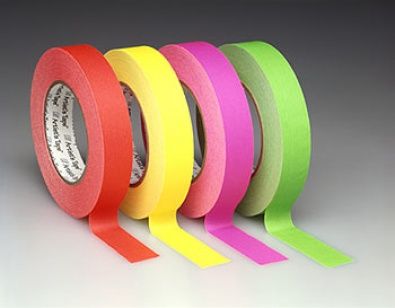
Fluorescent Colors Duct Tape