Sierra Conveyor Co., Inc.

Sierra Conveyor Co., Inc.
🇺🇸 United States, California
198011-50 peopleManufacturer/Service Company/DistributorSierra Conveyor Co., Inc., established in 1980 and headquartered in Rocklin, California, is a comprehensive full-line conveyor company and turnkey systems integrator. With over 40 years of industry experience, the company operates as a manufacturer, distributor, and service provider specializing in advanced material handling and automation solutions. Sierra Conveyor serves a diverse range of sectors, including Food & Beverage, Pharmaceutical, Retail & Apparel, E-Commerce, and 3rd Party Logistics, supporting high-profile clients such as Pepsico, Dell, and Hewlett Packard.
The company’s extensive product portfolio includes case, pallet, can, and bottle handling conveyors, as well as specialized systems such as spirals, sanitary conveyors, and robotic palletizing solutions. They offer a wide array of equipment types, including gravity, belt, live roller, and tabletop chain conveyors. Beyond standard equipment, Sierra Conveyor provides custom-engineered components, patented Quickfix Belts™, and on-site manufactured rollers. Their capabilities extend to complex automation, featuring Automated Storage and Retrieval Systems (AS/RS) and integrated sortation systems.
Sierra Conveyor provides end-to-end services from initial concepting and CAD-based engineering to fabrication, installation, and maintenance. They specialize in modifying existing systems, providing replacement parts, and offering expert repair services. As a versatile partner, they distribute products from leading brands like Dorner, Intralox, and Habasit, while also acting as a local distributor for Modular Conveyor Express (MCE). The company maintains a workforce of approximately 11 to 50 employees and generates an annual revenue between $5 million and $9.9 million.
Product customizationOffers full customization for design and features.
Established brandFounded in 1980, with over 20 years of industry experience.
Eco-friendly supplierUses sustainable and eco-friendly materials.
Contact
************
11
Products
Products
0
Categories
0
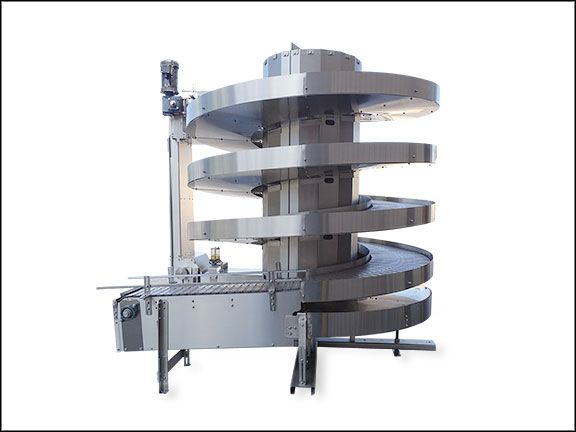
Spiral Conveyor - Spirex™
0·0 reviews
Conveyor Equipment
- Spirals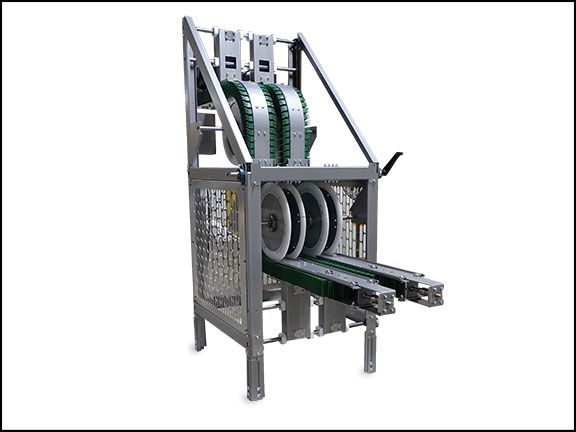
Gripper Elevator
0·0 reviews
Conveyor Equipment
- Vertical Conveyor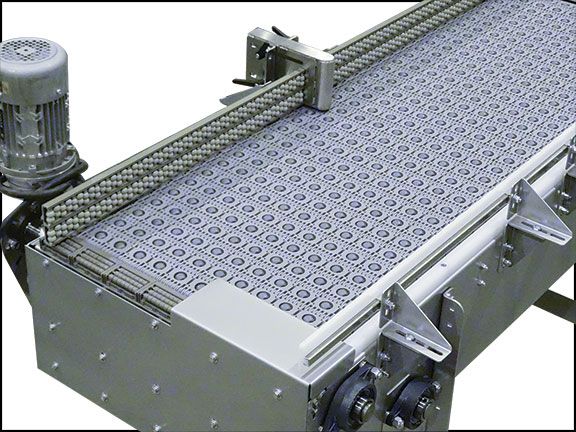
ARB™ Case Turner
0·0 reviews
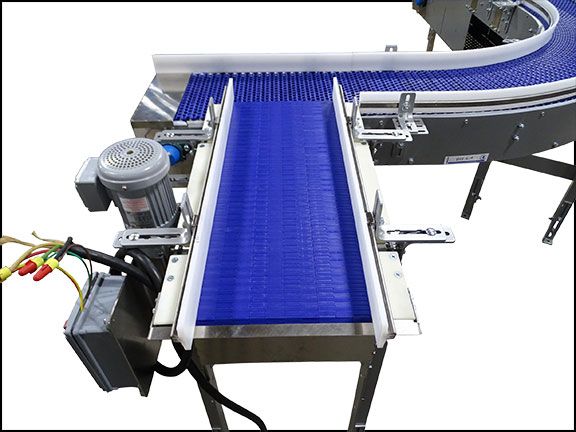
Micro-Transfer Conveyor
0·0 reviews
Conveyor Equipment
- Conveyor Transfers
MatTop Conveyor
0·0 reviews
Conveyor Systems
- MatTop Conveyor
Vertical Lift Conveyor
0·0 reviews
Conveyor Equipment
- Vertical Conveyor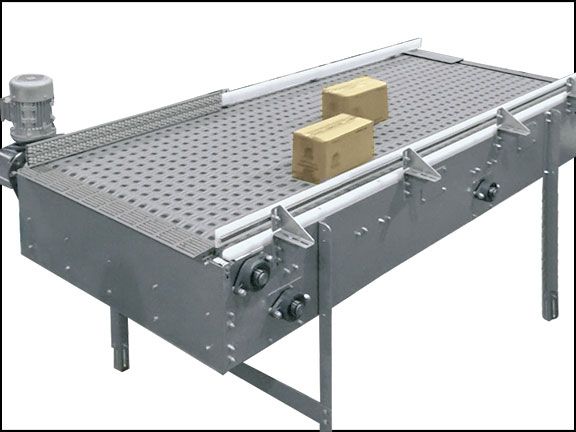
ARB™ Case Diverter
0·0 reviews
Conveyor Equipment
- Diverters & Laners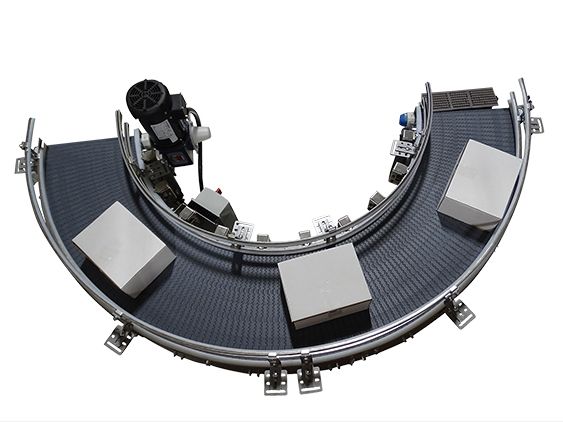
Zero Tangent Radius Conveyor
0·0 reviews
Conveyor Systems
- MatTop Conveyor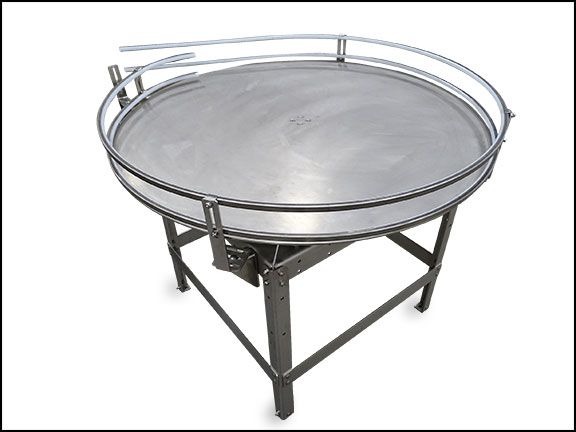
Rotary Accumulation Table
0·0 reviews
Conveyor Equipment
- Accumulators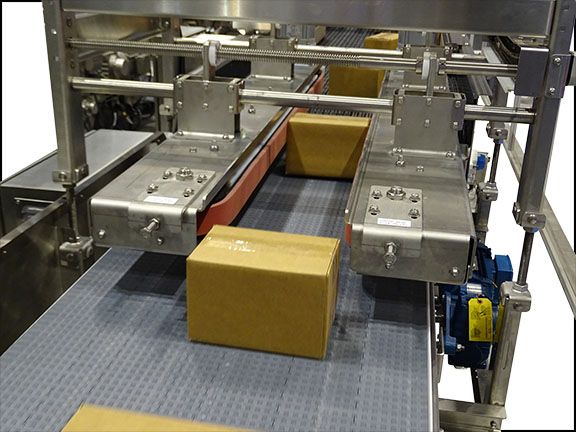
Side Belt Transfer
0·0 reviews
Conveyor Equipment
- Conveyor Transfers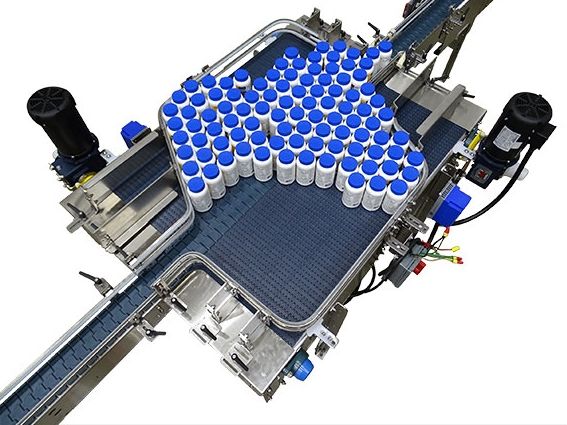
Re-Flow Accumulation Table
0·0 reviews
Conveyor Equipment
- Accumulators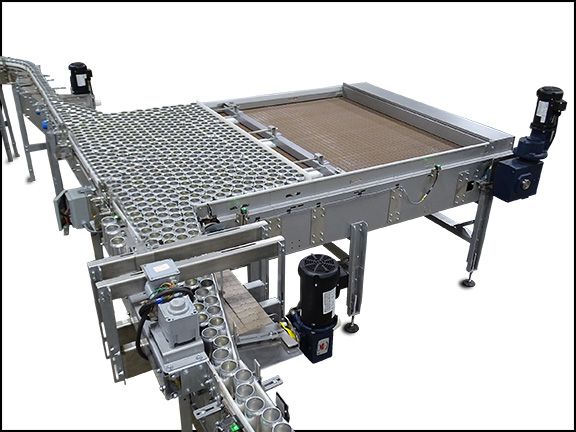
Bi-Directional Accumulation Table
0·0 reviews
Customers
ACSI
1
********
**********
****
*********
Unlock all 15 customers
Ask AI about this supplier
Similar suppliers you may like

Fluent Conveyors
🇺🇸 United States
201511-50 peopleManufacturer/Service CompanyProduct customization
Industry association member
OEM manufacturer
Shipments
1
Key customer
KALISCHATARRA
Key market
🇺🇸 United States
Description
Fluent Conveyors, founded in 2015 and based in Denver, Colorado, is a US-based manufacturer and service company specializing in custom conveyor systems and replacement parts. With 11-50 employees and an annual revenue of $4.6 million, the company operates through a strong dealer network across the United States, Canada, and Mexico. Fluent Conveyors offers a comprehensive range of conveyor solutions, including heavy-duty and light-duty roller chain conveyors, slider bed conveyors, trough idler conveyors, and various recycling sort systems. They also provide a full suite of replacement parts such as shafts, motors, pulleys, idlers, sprockets, and bearings, along with diverse replacement conveyor belts. Emphasizing high-end workmanship and bespoke material handling systems, Fluent Conveyors utilizes laser precision and the latest technology in their manufacturing processes. They offer OEM and ODM services, with products designed for industries including Bio-Fuel, Carpet Recycling & Processing, Construction & Demolition, OCC Recycling, Package Handling, and Waste Management. The company holds UL certifications and focuses on continuous innovation and customer satisfaction, providing pre-sales consultation and engineering services.
Ingalls Conveyors, Inc.
🇺🇸 United States
197611-50 peopleManufacturer/Trading Company/Service Company/DistributorEstablished brand
Product customization
Description
Ingalls Conveyors, Inc. is a premier manufacturer, distributor, and system integrator of material handling solutions based in Montebello, California. Founded in 1976, the company operates from a 174,000 sq. ft. facility and serves both local and nationwide markets. They specialize in the design, fabrication, installation, and modification of a wide range of conveyor systems, including gravity roller, belt, modular belt, food-grade, and live roller accumulation conveyors. As a direct distributor for major industry brands such as Hytrol and Southworth, the company provides both new equipment and high-quality reconditioned systems that are refurbished to meet "as new" warranty standards. Their extensive product portfolio also features pallet handling systems, spiral chutes, overhead track conveyors, scissor lifters, and electrical controls. Beyond equipment sales, Ingalls Conveyors offers comprehensive system integration for turnkey warehouse and manufacturing plant projects, supported by a fully equipped metal fabrication and welding shop for custom parts. For clients in Southern California, they provide specialized preventative maintenance and emergency repair services. The company is recognized for its ability to blend new and refurbished components to deliver cost-effective, engineered solutions tailored to specific industrial requirements.
Modular Belt Conveyors
Gravity Roller Conveyors
Belt Conveyors
Spiral Chutes
Food Grade Conveyors
Pallet Handling
Spiral Chutes
Lift & Tilts