Best Medical Equipment Suppliers in Canada
Discover reliable sourcing options for advanced medical equipment, including diagnostic tools, surgical instruments, and patient care technology from top-rated providers across Canada.
Medical EquipmentDiagnostic ToolsSurgical InstrumentsPatient CareHealthcare Technology

Kernic Systems Inc.
🇨🇦 Canada
197811-50 peopleService Company/Distributor/Trading CompanyEstablished brand
Product customization
Industry association member
Key market
🇨🇦 Canada
Description
Kernic Systems Inc. is a premier designer, integrator, and installer of complete material recovery and recycling systems headquartered in Burlington, Ontario, Canada. Founded in 1978, the company has over 40 years of experience providing economical and reliable solutions across North America and international markets. Operating through three primary divisions—Recycling Solutions, Dust Collection and Air Pollution Control, and Material Handling—Kernic Systems serves diverse industries including corrugated packaging, folding carton, tissue, printing, and post-consumer recycling.
The company specializes in a comprehensive range of industrial equipment, including auto-tie and vertical balers, shredders, air conveying systems, and advanced dust collection units such as wet scrubbers and oil & mist collectors. Through its 'OneSource™ for Simplicity' suite, Kernic Systems provides professional services encompassing custom engineering, project management, and factory-trained installation. They maintain strategic partnerships with global manufacturers like Maren Engineering Corporation, Bramidan Group, and Höcker Polytechnik GmbH to integrate high-quality components into their custom-engineered systems.
With a focus on safety and compliance, Kernic Systems ensures its solutions meet NFPA standards and other critical certifications like ISN and AICC. The company employs a skilled staff of 11 to 50 professionals, many with over 20 years of industry tenure, dedicated to optimizing throughput and maximizing waste-stream revenues for their clients. Their capabilities extend to providing both new and used equipment, as well as ongoing support through parts, maintenance, and industrial fire protection systems.
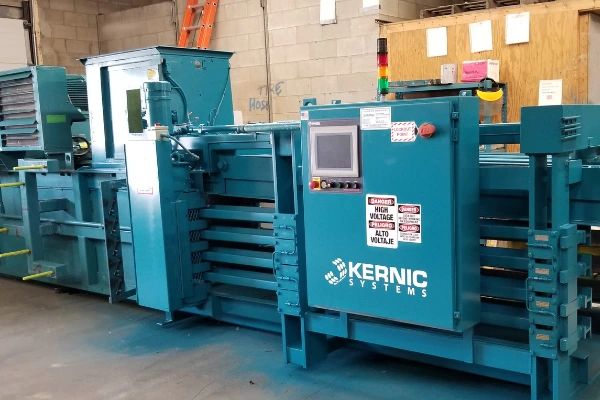
USED BALERS
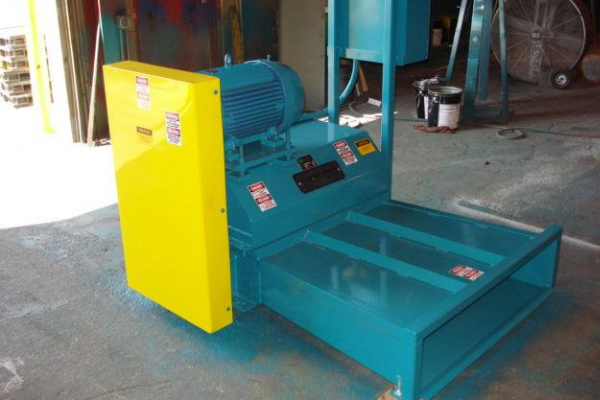
USED SHREDDERS
USED SHREDDERS
Samuel, Son & Co., Limited
🇨🇦 Canada
18555001-10000 peopleManufacturer/Distributor/Service CompanyHigh capacity factory
Established brand
Large enterprise group
OEM manufacturer
Key customer
NUGAR
Key market
🇲🇽 Mexico
Description
Samuel, Son & Co., Limited is a leading Canadian multinational manufacturer, processor, and distributor of metals and industrial products. Founded in 1855 and headquartered in Oakville, Ontario, the company has grown into one of North America’s largest metal service providers, operating over 70 facilities across Canada, the United States, and Mexico, with additional global operations in Europe and Asia. The company employs between 5,001 and 10,000 people and maintains an ISO 9001 certification, reflecting its commitment to high-quality standards and operational excellence.
As a comprehensive metal solutions provider, Samuel, Son & Co. offers an extensive inventory of carbon steel, stainless steel, aluminum, brass, copper, and aerospace alloys. These materials are available in various forms, including coils, sheets, plates, bars, tubes, and extrusions. The company’s advanced processing capabilities include precision laser and waterjet cutting, slitting, leveling, blanking, pickling, and heat treating. Beyond traditional metal distribution, the company has diversified into specialized industrial sectors through divisions such as Samuel Automation, which provides custom robotics and autonomous mobile robots (AMRs), and Burloak Technologies, which focuses on additive manufacturing and 3D metal printing.
Samuel, Son & Co. serves a wide range of industries, including automotive, aerospace, and energy. Its manufacturing portfolio features engineered products such as pressure vessels, railcars, and packaging systems. Supported by its own logistics arm, Kim-Tam Logistics, the company provides integrated supply chain solutions and just-in-time delivery to meet the complex requirements of its global B2B customer base.
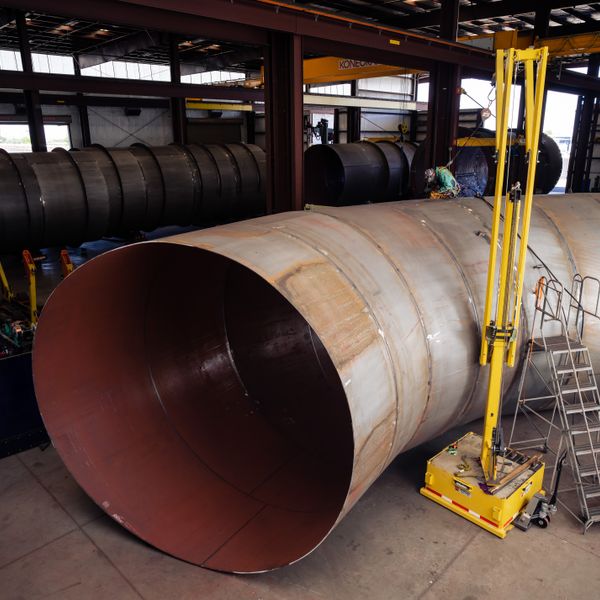
Advanced Fabrication
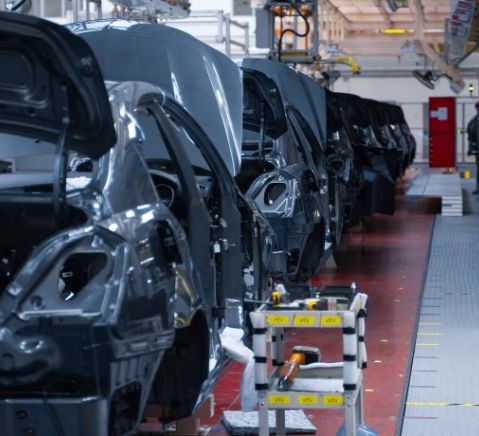
Automotive
T.D. Rooke Associates Limited
🇨🇦 Canada
197611-50 peopleDistributor/Service Company/WholesalerEstablished brand
Industry association member
Key customer
ASIMER GROUP
Key market
🇨🇦 Canada
Description
T.D. Rooke Associates Limited is a premier distributor and technical representative specializing in engineered process equipment solutions. Established in 1976 and headquartered in Concord, Ontario, the company serves a broad industrial base across Eastern Canada, including Ontario, Quebec, and the Atlantic provinces. Operating as a specialized wholesaler and service provider, the firm employs a team of skilled technical representatives to deliver high-quality fluid handling and processing equipment to the chemical, food and beverage, petrochemical, pharmaceutical, and water/wastewater industries.
The company's extensive product portfolio focuses on fluid processing and includes industrial mixers, agitators, centrifugal and metering pumps, heat exchangers, and advanced filtration systems. T.D. Rooke Associates Limited is an exclusive representative for globally recognized brands such as SPX Flow (LIGHTNIN, Philadelphia Mixers, Bran+Luebbe), ADMIX, Pick Heaters, SISTO Armaturen, and Eaton Filtration. Their offerings encompass specialized solutions like high-shear mixing, steam injection, sanitary diaphragm valves, and comprehensive dewatering equipment.
Beyond equipment supply, the company provides technical expertise and maintenance services, including mixer repair, custom fabrication, and preventative maintenance. With a professional team of 11 to 50 employees and decades of industry experience, T.D. Rooke Associates Limited supports clients in achieving operational efficiency through precision-engineered machinery and dedicated after-sales support.
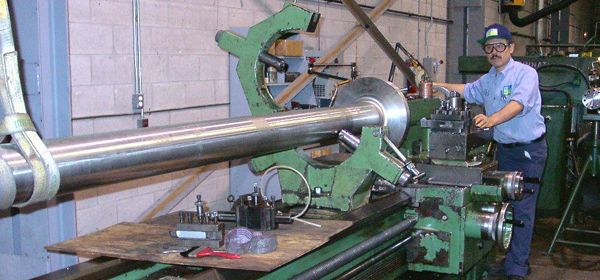
Custom Fabrication
Anamet Canada Inc.
🇨🇦 Canada
190811-50 peopleManufacturer/DistributorEstablished brand
Own brand
Product customization
Multinational enterprise
Key customer
HITACHI
Key market
🇧🇷 Brazil
Description
Anamet Canada Inc. is a premier manufacturer and distributor of specialized conduit systems for electrical cable protection, headquartered in Frankford, Ontario. With over 100 years of industry experience as part of the global Anamet Inc. group, the company operates state-of-the-art production facilities in Eastern Ontario. They are recognized as a leading Canadian provider of flexible conduits, manufacturing over 80% of their domestic product offerings locally. Their core portfolio includes the renowned Anaconda Sealtite liquid-tight flexible conduits, ANA-QUICK nylon conduit systems, and FIRETECH thermal protection solutions, such as heat-resistant sleeves, blankets, and tapes.
As an ISO 9001:2015 certified organization, Anamet Canada serves a diverse range of demanding industrial sectors, including power generation, food and pharmaceuticals, mass transit infrastructure, oil and gas, and OEM machine building. The company provides comprehensive solutions including conduit fittings, cable glands, and industrial stripwound hoses. Beyond standard products, they specialize in custom-engineered solutions, offering proprietary tooling for custom-colored jackets and specialized assemblies tailored to specific client requirements. Their products meet rigorous international standards, including UL, CSA, ATEX, and RoHS compliance. With a dedicated team of approximately 35 professionals and a robust national distribution network, Anamet Canada combines local technical support with a global reach, exporting to markets across North America, Europe, and South America.
Anaconda Sealtite® Liquid Tight Flexible Conduit
How many suppliers does SourceReady track globally?
SourceReady tracks 4.0M+ suppliers globally across 200 sourcing countries and 7,000+ product categories.

Pyromaitre Inc.
🇨🇦 Canada
198111-50 peopleManufacturerEstablished brand
Product customization
OEM manufacturer
Industry association member
Key customer
RASSINI
Key market
🇨🇦 Canada
Description
Pyromaitre Inc. is a specialized Canadian manufacturer of high-precision industrial ovens and thermal processing equipment, headquartered in Levis, Quebec. Founded in 1981, the company has over 30 years of expertise in mastering heat transfer and convection technology. Pyromaitre serves a global clientele across more than 25 countries, providing advanced solutions for the automotive, aerospace, and medical industries, with a notable customer base including Ford, Toyota, and Bombardier.
The company specializes in high-speed tempering and stress-relieving ovens designed for parts such as springs, wireforms, shafts, and bearings. Their product portfolio includes electric, gas, and custom-made conveyor ovens, as well as specialized cooling chambers like the PyroCool, recirculating coolers, and waterspray coolers. A key differentiator of their technology is the ability to reduce heat treatment cycle times by 3 to 10 fold, while decreasing floor space requirements by up to 70% and energy consumption by 25%.
As an OEM manufacturer, Pyromaitre operates a factory capable of high-volume production, such as processing 30,000 lbs of suspension springs per hour. Their equipment is CQI-9 compliant and features the proprietary Pyrograph software for precise temperature control. In addition to manufacturing, they offer R&D services, rental and leasing programs, and comprehensive maintenance support. Recognized for engineering excellence, the company was awarded Industrial Ovens Manufacturer of the Year 2024.
Velan Inc.
🇨🇦 Canada
19501001-2000 peopleManufacturer/Trading Company/DistributorHigh capacity factory
Established brand
Large enterprise group
Patented technology
Key customer
VELAN
Key market
🇮🇳 India
Description
Velan Inc. is a world-leading manufacturer of industrial valves headquartered in Montreal, Canada. Founded in 1950, the company has grown into a global leader with over 1,200 employees and a manufacturing footprint of 90,000 m² across 11 production facilities worldwide. As a publicly traded company (TSX: VLN), Velan specializes in the design and production of a comprehensive portfolio of industrial valves, including gate, globe, check, ball, triple-offset, butterfly, and severe service valves, as well as steam traps and automation solutions. Their products are engineered for demanding applications across critical sectors such as nuclear power, oil and gas, mining, chemical, and marine industries.
The company is recognized for its advanced engineering capabilities, offering valves in sizes ranging from 1/2” to 64” and pressure ratings up to ASME Class 4500. Velan holds ASME certifications and is a key supplier for high-stakes environments, including cryogenic, high-temperature, and corrosive applications. Beyond manufacturing, they provide extensive aftermarket services, including OEM spare parts, valve repair, and maintenance. With a robust global supply chain and a commitment to innovation, Velan serves major international clients such as Ontario Power Generation and Bruce Power, maintaining a strong focus on quality and safety in the flow control industry.

Cortex Design Inc.
🇨🇦 Canada
199911-50 peopleService CompanyEstablished brand
ODM manufacturer
Product customization
Industry association member
Key customer
3M
Key market
North America
Description
Cortex Design Inc. is an award-winning product design and engineering firm headquartered in Toronto, Canada. Founded in 1999, the company operates as a specialized service provider with a team of 11 to 50 professionals, focusing on the development of complex medical devices and consumer electronics. They are distinguished by their dual certification in ISO 13485:2016 and ISO 9001:2015, ensuring high-quality standards for regulated industries.
The firm utilizes a proprietary Design for Commercialization™ methodology to guide clients through the entire product lifecycle, from initial concept to market launch. Their comprehensive service suite includes industrial design, mechanical engineering, hardware and PCB design, embedded firmware development, and microfluidics. Cortex Design specializes in high-growth sectors such as wearables, point-of-care diagnostics, IoT devices, and life science instruments.
Beyond design and engineering, the company provides robust manufacturing support, including assembly, production management, and overseas manufacturing liaison services. They leverage advanced technical capabilities such as thermal simulation, CAD modeling, and human-centered design to optimize product performance. Cortex Design serves a diverse global clientele, ranging from innovative startups to established multinational organizations like 3M, Deloitte, and Laborie.
Fuller Industrial Corp
🇨🇦 Canada
200451-100 peopleManufacturer/Service Company/DistributorEstablished brand
Product customization
Patented technology
Key customer
AURELIAN
Key market
🇪🇨 Ecuador
Description
Fuller Industrial Corp is a Canadian manufacturer, service company, and distributor based in Lively, Ontario, specializing in comprehensive process piping solutions. Established in 2004, the company employs 51-100 people and generates an annual revenue of $14.2 million. Fuller Industrial offers end-to-end services from design and supply to maintenance, with a strong focus on engineered piping systems, pipe spool fabrication, and wear product solutions. Their expertise includes rubber lining, ceramic lining, industrial coatings, and advanced 3D pipe design for abrasion and corrosion control. They provide customized prefabricated piping, along with the distribution of pipes, valves, fittings, pipe supports, and hoses. Fuller Industrial serves diverse heavy industries such as mining, oil & gas, agriculture, and manufacturing, aiming to maximize client profitability through cost savings, increased uptime, and simplified project management. The company operates a factory and offers contract manufacturing services, emphasizing quality, transparency, and efficient processing. They also provide Leak Prevention technology for real-time wear detection and predictive maintenance. Fuller Industrial has completed over 50 projects and supported more than 100 plants, positioning itself as an international partner with advanced fabrication and lining capabilities in North America.
AMF Industries Inc.
🇨🇦 Canada
20185-10 peopleDistributor/Service CompanyKey customer
BON TOOL
Key market
🇺🇸 United States
Description
AMF Industries Inc. is a specialized distributor and service provider of industrial components and process automation solutions based in Labrador City, Canada. Founded in 2018, the company operates multiple locations in Eastern Canada, including Montreal, and serves a diverse range of sectors such as mining, water and wastewater treatment, aerospace, power generation, and oil and gas. The company maintains a strong focus on technological leadership and quality, offering a comprehensive portfolio that includes industrial filtration, instrumentation, and valves and controls. Their extensive product range features flowmeters, actuators, pressure regulators, sensors, hydraulic power units, and various industrial fittings. AMF Industries Inc. represents leading brands such as Badger Meter, Bonomi, Bray, and DeZurik, providing technical support and training to ensure efficient process automation for their clients. The company's commitment to industry standards is reflected in their offering of products that meet CE, CSA, UL, and ASME certifications. With a team of process automation professionals, they provide end-to-end support for complex industrial projects, particularly within the mining and water treatment industries.
Alfa Laval Inc.
🇨🇦 Canada
1976101-200 peopleManufacturer/Service Company/Trading CompanyEstablished brand
OEM manufacturer
Product customization
Patented technology
Key customer
ALFA LAVAL
Key market
🇲🇽 Mexico
Description
Alfa Laval Inc. is a leading manufacturer and service provider specializing in heat transfer, separation, and fluid handling technologies. Operating in Canada for over 120 years, the company serves as a critical subsidiary of the global Alfa Laval group, which was founded in 1883. Headquartered in Scarborough (Toronto), Ontario, the Canadian division employs over 100 professionals, including industrial technicians and engineering experts, and maintains specialized repair facilities in both Toronto and Edmonton. The company is a certified manufacturer with ISO 9001, FDA, 3A, and EHEDG standards, reflecting its commitment to quality and safety across highly regulated industries.
Their extensive product portfolio includes plate and brazed heat exchangers, centrifugal separators, decanter centrifuges, and a wide range of fluid handling equipment such as industrial pumps, sanitary valves, and tank cleaning systems. Alfa Laval Inc. provides essential solutions for diverse sectors, including food and beverage, dairy, biotech, pharmaceuticals, HVAC, marine, and wastewater treatment. Beyond equipment manufacturing, they offer comprehensive lifecycle support, including 24/7 technical service, local repair, and specialized maintenance for industrial centrifuges and heat exchangers.
As a pioneer in sustainable engineering, the company focuses on energy efficiency and environmental compliance. Key offerings include ballast water treatment systems, marine boilers for maritime decarbonization, and advanced sludge dewatering equipment for municipal and industrial operations. Through its global network and local Canadian presence, Alfa Laval Inc. enables businesses to optimize thermal processes, reduce pollution, and enhance productivity through innovative separation and fluid handling technology.
FAQ
Can I search for suppliers using one sentence?
Can enterprise teams use SourceReady for supplier research?
Can I save suppliers to a custom list?